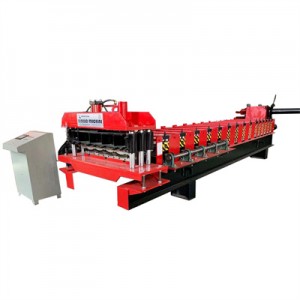
Roofing tile roll forming machine and metal tile roof former, supplied factory direct by the manufacturer to steel building projects in the Middle East.
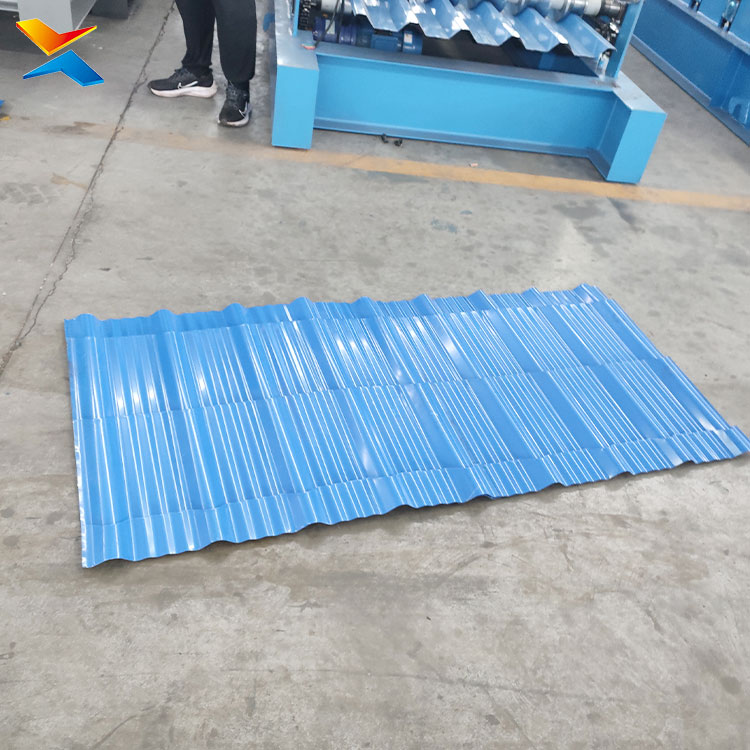
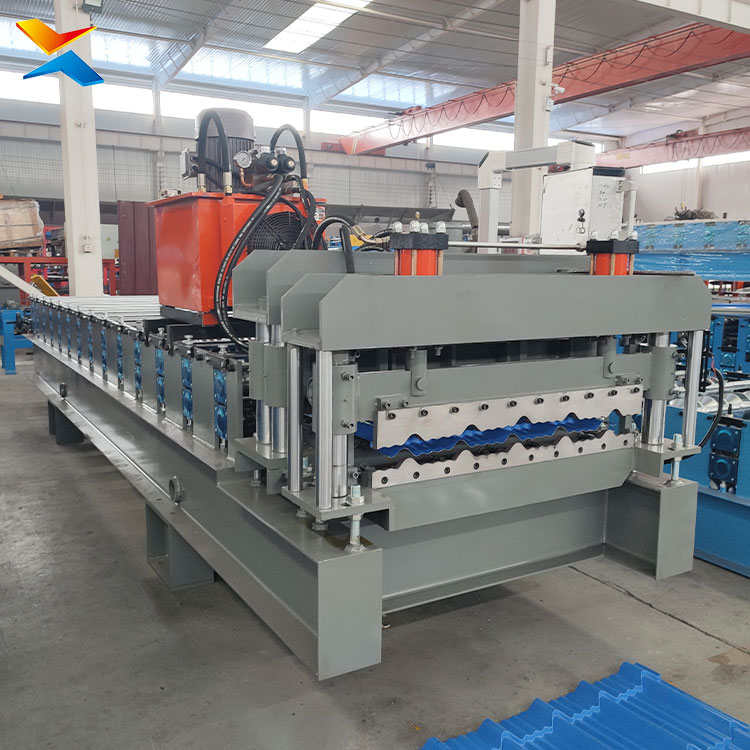
The machine forms coated steel coil into metal roof tile panels. The arc of the tile is formed progressively across a train of roll stands, a pitch-stamping device divides that arc into tile courses along the panel’s length, the side edges are formed so that one panel laps into the next, and the panel is cut to the length the roof requires.
The price of a tile roll former is a configuration, not a figure.
“Roofing tile roll forming machine” names a family, not a product. Within that name sit machines that differ in how many roll stands they carry, how heavy their frames are, whether the pitch device is mechanically timed or servo-positioned, how wide a panel they form, what tooling they include and what is delivered with them. Two machines that both answer to the name correctly can differ substantially in what they cost, because they are not the same machine.
That is why no figure is printed here. A price is the sum of the decisions below, and a number quoted before those decisions are made is not a price for this machine — it is a price for a different machine that happens to share the name.
How the cost of the machine is built up.
The number of forming passes. The arc is not struck in a single pass; it is accumulated across the stands, and the deeper the arc the more stands are needed to reach it without marking or over-straining the strip. Pass count is therefore the first cost driver, because each additional stand adds a pair of rolls, a pair of shafts, a housing, a bearing set and length to the frame. A deep-arc profile is a longer and heavier machine than a shallow one before anything else is decided.
The pitch die set. The pitch device carries tooling that is designed for one pitch. The die set is not an adjustable approximation of a pitch; it is made for it. A pitch that already exists in the manufacturer’s archive is a known tooling item. A pitch outside the archive is new engineering and new tooling, and that work is a cost item in its own right rather than a setting to be dialled in.
The frame class. The frame has to carry both the forming load of the profile and the mass of the stands without deflecting, so frame section and mass rise with the width and depth of the panel being formed. A frame that is light for its profile shows up as an arc that varies along the length, which is a quality failure rather than a saving.
The drive arrangement. In the standard arrangement the pitch device is driven from the main transmission through a chain or gear train. In the servo arrangement the pitch device is positioned by its own motor, with the forming drive carried through a bevel gearbox so the two are controlled separately. The servo arrangement adds a motor, a drive, an encoder and the control logic that ties them together, and it buys regularity of the course spacing that the mechanical arrangement cannot hold over a long panel.
The cutting unit and its control. The panel is cut after forming, at a position related to the pattern, so that a panel ends on a course line. The cutting arrangement and its control are part of the machine’s cost, and a cutting arrangement that cannot repeat its position leaves a different length at the eave on every panel.
Tooling options. A dual-width version needs additional tooling to produce a second panel width. A multi-material version needs tooling engineered for both coated steel and resin tile material, because the two materials behave differently in forming. Each of these is a tooling cost before it is anything else.
The scope delivered with the machine is part of its price.
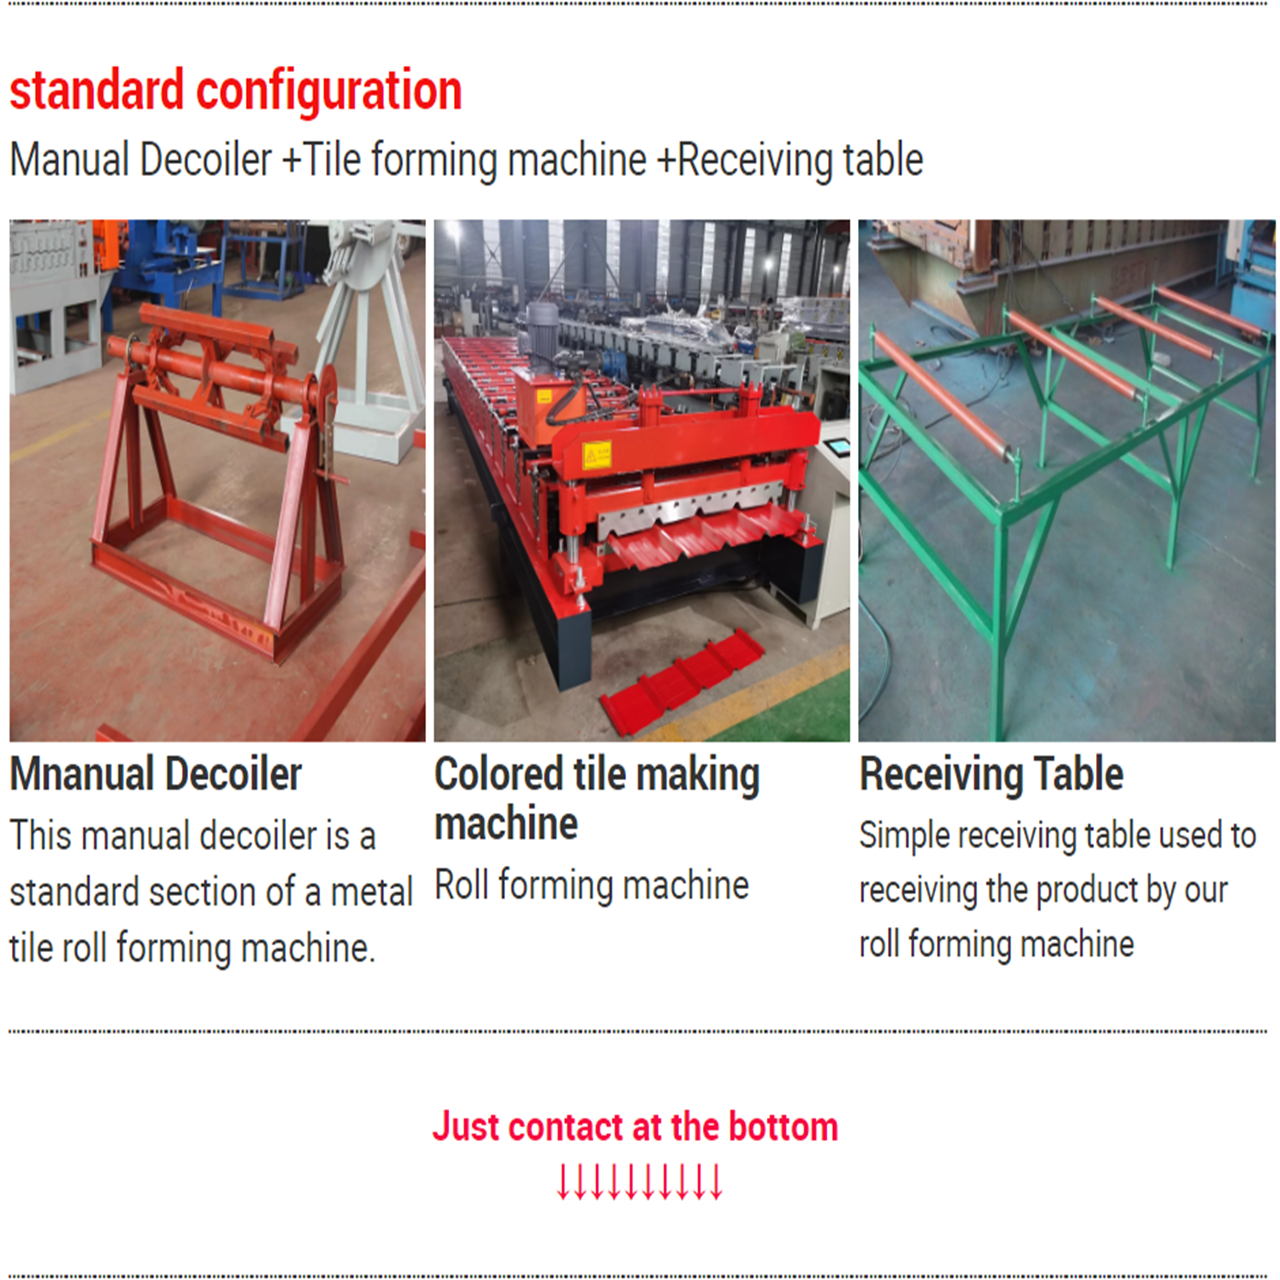
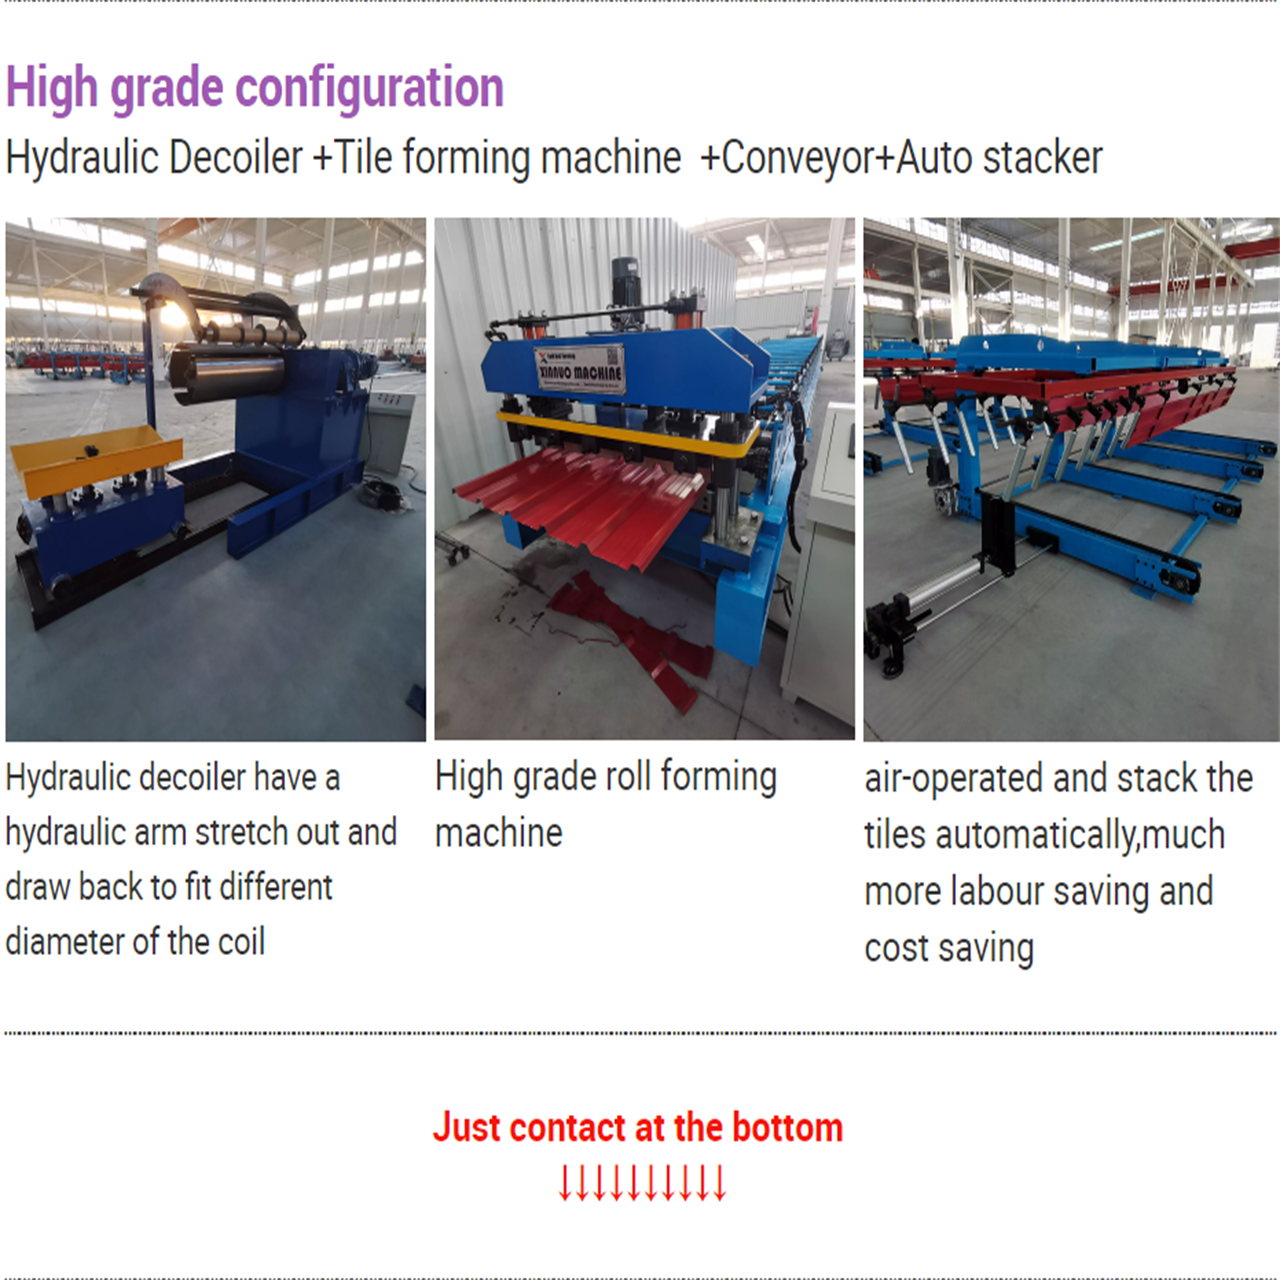
A tile roll former is not bought as a bare machine. What travels with it — the decoiler that carries the coil, the run-out that receives the finished panel, the control system, the illustrated manuals, the operator training, the commissioning support and the spare parts list — is part of what the price is paying for.
Two quotations that both read “roofing tile roll forming machine” can therefore differ substantially without either being wrong, because the delivered scope differs. The comparison only becomes meaningful when the scope is written down beside the figure: which units are included, what the tooling covers, what support is provided and what is excluded.
What the machine’s price does not include.
The steel coil. The machine forms the buyer’s coil; it does not supply it. Coil is the raw material and it is procured separately, and its grade, coating and thickness are a cost of the roof rather than of the machine. Treating the coil as part of the machine’s price is one of the ways a project’s budget is misread.
The roof accessories. The ridge, the hip, the verge and the eave details are formed to the panel’s profile, and they come from their own tooling. A project that needs a complete roof needs the accessory tooling as well as the panel tooling, and the two are separate items.
Freight, insurance and duty. These depend on the destination, the mode and the route, and they are not part of the machine’s ex-works cost.
Site works. The foundation, the power supply to the machine, the lifting equipment and the building’s clear height are site costs. On a double layer machine the height matters, because the upper roller set has to be reached for tooling changes.
Why the figure that matters is the landed cost.
A tile roll former is a long and heavy machine, and its freight volume follows its length and its frame. A machine with more forming passes is a longer machine, and a heavier frame adds mass, so the configuration that costs more at the works also occupies more space in a container and weighs more in transit.
For a project in the Gulf, the number that has to be compared is therefore not the figure at the works but what arrives on site: the machine, its scope, its tooling, and the freight that brought it. A lower figure at the works that needs an extra container, or that arrives without the decoiler, is not a lower cost to the project.
Why a lower figure for the same profile is normally a different machine.
When two suppliers quote the same nominal profile at figures far apart, the difference is rarely in the margin. It is usually in one of the cost drivers above: fewer forming passes, a lighter frame, a mechanically timed pitch device instead of a servo one, a narrower delivered scope, or accessory tooling that is not included.
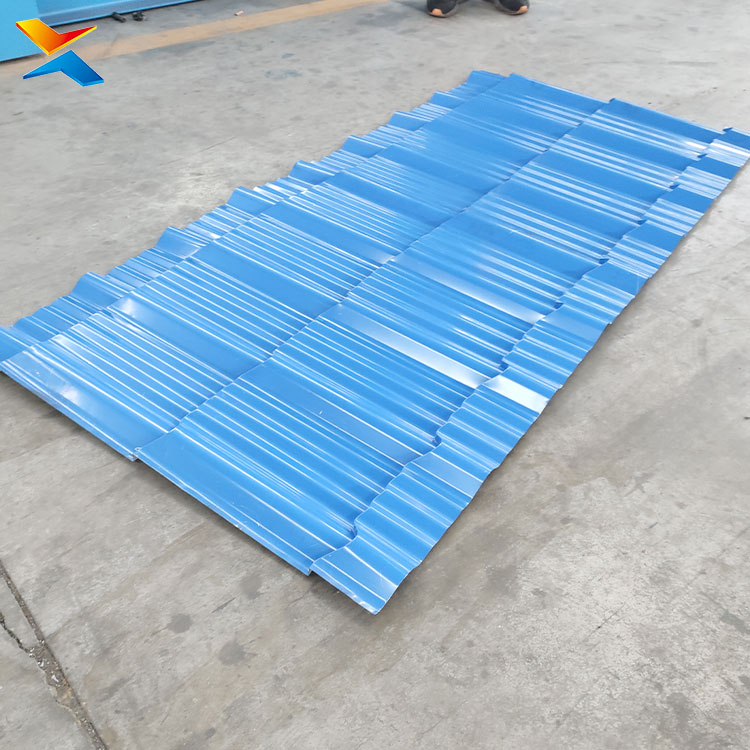
None of those differences is visible in the profile’s outline, because the outline is the same in every case. What shows them is the panel: whether the arc holds its shape along the full length, whether the course spacing stays regular from the first tile to the last, and whether the panel ends on a course line at the eave. The panel is the evidence of what was bought.
What the machine is, in production terms.
The coil is paid off and guided square into the first stand. The arc is formed progressively across the stands. The pitch device presses a division into the crest at each tile pitch, turning a continuous arc into a sequence of tile courses. The side profiles are formed so that one panel laps into the next and the joint closes. The panel is cut to length at a position related to the pattern, and it leaves the machine on a support that keeps it from being dragged or twisted as it comes off.
The pitch families and their cost position.
A pitch that exists in the manufacturer’s archive is a known die set, and its cost is the cost of that tooling. A pitch that does not exist in the archive is a new engineering item: the die set has to be designed, made and proved against the panel, and the proving is part of the work.
That is why the tile idiom a project chooses is also a commercial decision and not only an architectural one. A fine pitch with closely spaced courses, a mainstream medium pitch, a broad deep-arc pitch, a bamboo-joint relief, an asymmetric arc, a ribbed variant or a half-course edge — each has its own tooling position, and the ones already in the archive are the ones that can be quoted against a drawing rather than developed from nothing.
Configurations.
Standard single-profile machine. One set of tooling, one profile, one thickness range, with the pitch device mechanically timed.
Servo-driven pitch control. The pitch device positioned by its own motor, with the forming drive through a bevel gearbox, for regularity of course spacing across long panels and between production runs.
Dual-width version. Additional tooling that produces two panel widths.
Multi-material version. Tooling engineered for both coated steel and resin tile material.
Higher-power build. A heavier drive and frame for the deeper and wider profiles and for higher line speeds.
Machine construction.
The frame is machined so that the stands sit in line and hold their centres, because the arc is the sum of what every stand does. The forming rolls are made in pairs, hardened, ground and finished so the working surface holds its shape. The shafts are alloy steel, ground, and sized to the load the profile imposes. The pitch die set is made for the pitch rather than adjusted to it. The structures are welded under shielding gas, stress-relieved where the design calls for it, shot-blasted, and finished with an electrostatic coating cured in an oven.
Product features and advantages.
Formed to the project’s drawing. The panel is produced to the profile, pitch, panel width, lengths and material the building was designed with, so the roof on the drawing is the roof the tooling is set to.
Pass count matched to the arc. The number of forming stands follows the depth of the arc rather than a fixed pattern, so a deep profile is formed gradually instead of being forced.
A pitch die set made for the pitch. Each pitch in the archive has its own designed tooling, which is what holds the course spacing and the depth of the division across a production run.
Fixed at the crest and hidden by the lap. The profile places the fastener in the crest, where the following panel’s overlap covers it, leaving a finished roof with no exposed fixing.
Half-course edges for whole-panel coverage. Two panels form one complete course across the joint, so a roof plane is covered in whole panels and finishes on a course line.
Course-line cutting. The panel is cut relative to the pattern, so a panel ends on a course rather than through a tile.
Ribbed variants for walked roofs. Additional stiffening ribs raise the panel’s stiffness without changing its tile reading.
A scope that is written down. The delivered scope — units, tooling, support and exclusions — is stated with the configuration, because that is what the figure is paying for.
Middle East supply.
The machine is supplied into the Gulf markets, including the United Arab Emirates, Saudi Arabia, Qatar, Oman, Kuwait and Bahrain, for villa compounds, mosques and religious buildings, hotel and resort roofs, showrooms and commercial frontages, heritage-style steel-framed buildings, and the canopies, gate structures and pavilions that surround them.
Two things make the region specific for a machine of this kind. The first is the roof’s exposure: coastal cities work under humid, salt-bearing air for much of the year, while inland cities work under dry heat, hard sun and wind that carries sand. A coated panel is protected only while its coating is continuous, and every cut edge and every fastener is a break in it, so the coil’s coating and the quality of the forming that must not crack it carry more weight on a Gulf roof than the profile’s outline does.
The second is logistics. The machine travels by sea to a Gulf port and then inland, so its length, its mass and the volume it occupies are commercial facts rather than details. A configuration with more stands and a heavier frame is a better machine and a larger shipment, and both sides of that belong in the same decision.
Conditions the panel meets on a Gulf roof.
Heat and thermal movement. The panel runs well above air temperature and moves across its length accordingly, so fixings and end details have to let it move rather than hold it rigid. The colour and gloss a roof keeps over its life are a property of the coating, not of the profile.
Dust and wind-blown sand. The course divisions that give the panel its tile appearance are also where dust settles and where a cleaning brush has to reach. Deeper relief reads more strongly and holds more dust, and the two are chosen together on a dusty site.
Salt air at the coast. Corrosion starts at the cut edges, the fasteners and the ends of the laps, because those are where the coating is interrupted.
Short intense rain. Total rainfall is low but heavy when it comes, so the roof has to clear a large volume quickly, and the profile’s pans are the path that water takes to the eave.
Where the panel is used.
Villa roofs and villa compounds; mosques and religious buildings; hotel and resort roofs with their pavilions, canopies and gate structures; showrooms and commercial frontages where the roof is part of the elevation; heritage-style and new-classical buildings on steel frames; entrance canopies, guard structures, gazebos and poolside buildings; feature walls and screens carrying the same tile reading down the façade.
Service and support.
The machine is supplied with installation and commissioning support, operator training, illustrated manuals and a spare parts list, and with engineering support for the profile a project requires. Because the pitch tooling is specific to one pitch, the tooling record is part of what is handed over: it is what allows the same panel to be produced again for a later phase of the same project, and it is what makes the second order a repeat rather than a new development.
Factory direct.
The machine is built by the manufacturer and supplied directly, with no trading intermediary between the works and the buyer. The tooling comes out of the manufacturer’s own archive of tile and arc profiles, so a profile already in that archive is a known item with a known die set, and the configuration behind the figure is one that can be described, checked and delivered.
♦ COMPANY PROFILE:
Hebei Xinnuo Roll Forming Machine Co., Ltd., not only produce different types of professional roll forming machines, but also develop intelligent automatic roll forming production lines, C&Z shape purline machines, highway guardrail roll forming machine lines, sandwich panel production lines, decking forming machines, light keel machines, shutter slat door forming machines, downpipe machines, gutter machines, etc.
There are several advantages of using roll forming for your projects:
- The roll forming process allows operations such as punching, notching, and welding to be performed in-line. Labor cost and time for secondary operations are reduced or eliminated, reducing part costs.
- Roll form tooling allows for a high degree of flexibility. A single set of roll form tools will make almost any length of the same cross-section. Multiple sets of tools for varying length parts are not required.
- It can provide better dimensional control than other competing metal forming processes.
- Repeatability is inherent in the process, allowing easier assembly of roll formed parts into your finished product, and minimizing problems due to “standard” tolerance build up.
- Roll forming is typically a higher speed process.
- Roll forming offers customers a superior surface finish. This makes roll forming an excellent option for decorative stainless steel parts or for parts requiring a finish such as anodizing or powder coating. Also, texture or pattern can be rolled into the surface during forming.
- Roll forming utilizes material more efficiently than other competing processes.
- Roll formed shapes can be developed with thinner walls than competing processes
In modern construction and manufacturing, the roll forming machine (commonly known as a roof tile or sheet metal roll former) has revolutionized profile fabrication. By replacing labor-intensive traditional press brake methods, advanced roll forming technology offers unmatched efficiency, quality, and cost savings for metal roofing and wall panel production.
Here are the key advantages of implementing a modern roll forming machine in your operations:
1. Unmatched High Efficiency and Output Speed
High-speed roll forming lines operate continuously, producing custom metal panels at speeds up to 20–40 meters per minute. This automated process significantly shortens lead times and accelerates project delivery cycles.
2. High Precision and Consistent Quality
Engineered with heavy-duty steel frames, high-precision roller dies, and PLC automated control systems, roll formers deliver pinpoint dimensional accuracy. Every panel exhibits uniform thickness, sharp profiles, and precise hole punching, ensuring seamless job-site installation.
3. Material Efficiency and Reduced Waste
Continuous roll forming minimizes scrap metal generation compared to conventional stamping. Precise coil feeding and automated hydraulic flying shears ensure optimal material utilization and reduced raw material costs.
4. Low Maintenance and Extended Durability
Constructed with heat-treated chrome-plated rollers and robust drive systems, industrial roll forming machines require minimal downtime while delivering a long service life under heavy daily operation.
Conclusion
Investing in a reliable roll forming machine boosts productivity, lowers labor costs, and guarantees consistent product quality—delivering maximum long-term return on investment (ROI) for metal fabrication businesses.
Metal roll forming is a continuous, automated metal fabrication process used to shape long strips of sheet metal (usually coiled steel or aluminum) into specific, uniform cross-sectional profiles.
Unlike traditional metal bending techniques like press braking—which shapes sheets batch by batch—roll forming operates as a continuous production line, making it one of the most efficient manufacturing methods for structural profiles, roofing panels, and automotive components.
How the Metal Roll Forming Process Works
The process passes coil stock through a series of consecutive roller dies to incrementally shape the metal into a finished cross-section:
-
Uncoiling: A heavy coil of sheet metal (often pre-painted, galvanized, or stainless steel) is mounted onto a decoiler and fed continuously into the line.
-
Progressive Forming: The strip passes through a sequence of mating roller stations (known as flower patterns). Each set of rollers gradually bends the metal by a few degrees. By making incremental bends, the process avoids overstressing the material or cracking protective coatings.
-
In-Line Processing (Optional): Pre-punching, post-punching, slitting, or embossing can be integrated directly into the automated line before or after forming.
-
Cutting to Length: Once the final profile is shaped, an automated flying shear or hydraulic cutter cuts the continuous panel into precise custom lengths without interrupting the line speed.
Key Advantages of Metal Roll Forming
-
Continuous High Output: Roll forming lines operate at high speeds (typically 20–50 meters per minute), significantly outperforming press brakes for mass production.
-
Tight Dimensional Tolerances: Advanced PLC automation and precision-machined rollers ensure strict dimensional consistency across every piece produced.
-
Material & Cost Efficiency: Minimizes scrap metal waste and eliminates extra handling steps by integrating punching, bending, and cutting into a single automated line.
-
Design Flexibility & Surface Protection: Capable of producing complex, multi-bend profiles while preserving surface finishes, galvanization, and paint coats.
Common Applications
Metal roll forming is widely used across multiple heavy-duty industries:
| Industry | Common Roll-Formed Products |
| Building & Construction | Trapezoidal roof tiles, standing seam panels, C/Z purlins, drywall studs, rain gutters |
| **Automotive &# What is Metal Roll Forming? |
Metal roll forming is a continuous, high-volume manufacturing process that bends long strips of sheet metal—usually coiled steel or aluminum—into custom cross-sectional profiles.
Unlike traditional press braking or stamping, which processes metal in single discrete batches, roll forming shapes metal incrementally at room temperature (cold forming) through a series of consecutive roller dies.
How Metal Roll Forming Works
The roll forming process relies on a line of paired roller stations that gradually shape the metal in steps:
-
Coil Unloading & Uncoiling: A heavy coil of flat metal strip is loaded onto an uncoiler and fed continuously into the machine.
-
In-Line Pre-Punching: Automatic presses notch, punch holes, or create slots in the flat strip prior to shaping.
-
Progressive Roll Shaping: The strip passes through multiple sets of upper and lower rollers (called roll stations). Each station bends the metal slightly more than the previous one, preventing stress fractures and material strain.
-
Cutting & Shearing: A flying hydraulic shear cuts the finished profile to exact target lengths without stopping the continuous line.
Key Benefits of Roll Forming
-
High Speed & Efficiency: Lines operate at speeds up to 20–50 meters per minute with minimal manual labor required.
-
Consistent Quality & Precision: Heavy-duty tool steel rollers controlled by PLC automation ensure exact tolerances across thousands of identical panels.
-
Material Waste Reduction: Continuous coil processing generates virtually zero scrap compared to conventional sheet stamping or trimming.
-
Complex Profiles: Produces intricate shapes—such as standing seam panels, hat channels, C/Z purlins, and tubular sections—in a single continuous pass.
Common Applications
-
Building & Construction: Roof tiles, wall cladding panels, gutters, structural purlins, and steel framing studs.
-
Automotive: Bumper beams, door impact bars, and chassis structural rails.
-
Solar & Energy: Solar panel mounting racks and support structures.
-
Storage & Industrial: Warehouse racking systems, shelving, and heavy-duty tracks.