Plate shearing machine — hydraulic guillotine shearing machine for steel fabrication work in Saudi Arabia. The machine shears steel plate of substantial thickness into rectangular blanks with a straight, square edge in a single cutting stroke. It is built by the manufacturer and supplied for the plate-cutting stage of steel fabrication, where the blank that leaves the shear is the starting point for forming, fitting and welding.
The machine is a guillotine type shear driven by hydraulics. A long straight upper blade descends through the plate against a fixed lower blade and cuts it along a straight line across the full width of the machine. The plate is clamped flat and still by a row of hold-downs beside the cutting line, the blade angle and the blade gap are set to suit the material, and the cut length is set by a back gauge that positions the plate repeatably. The whole machine is built on a heavy welded frame, and the rigidity of that frame is what keeps the cut edge square.
The machine in a steel fabrication shop.
Steel fabrication is the business of turning steel stock into finished structures and equipment: plate and sections are cut to size, formed, assembled, welded, and finished into tanks, vessels, skids, platforms, frames, ducting, structural steelwork and machine bases. The work is organized around a sequence that begins with cutting, and in a plate fabrication shop that first operation is usually a shearing machine.
The shear’s job in that sequence is to produce plate blanks that are the right length and square. That is a narrower job than it looks, and it is more important than it looks. Every operation downstream works from the blank: a plate that is cut long has to be trimmed or re-cut; a plate that is cut out of square throws the assembly out before a weld is laid; and a plate whose edge is not clean has to be dressed before it can be fitted. The shearing machine determines the length and the squareness of the blank, and therefore the shearing machine is where the accuracy of the whole fabrication sequence is set.
That is why the machine is built around four things rather than around cutting force alone: the rigidity of the frame, the control of the blade through the cut, the firmness with which the plate is clamped, and the repeatability of the cut length.
Working principle.
The machine shears rather than saws or burns. The upper blade is carried in a blade beam and driven downward by hydraulic cylinders; the lower blade is fixed in the bed. The descending upper blade and the stationary lower blade pass each other with a small clearance and the plate is sheared along that line through its full thickness.
Hydraulic drive gives the machine its working flexibility. Cutting force is developed by oil pressure from a hydraulic power unit, so the machine can be set for the material in front of it. The angle at which the upper blade enters the plate is adjustable, and the clearance between the upper and lower blades — the blade gap — is adjustable to suit the plate thickness. A blade entering at a suitable angle with a suitable gap shears the plate cleanly through its thickness, and the stroke is steady and smooth. After the cut the blade beam returns to its raised position, ready for the next plate.
Machine construction — the main assemblies.
The frame. A heavy welded steel structure with thick side plates and a rigid bed. The frame carries the full cutting force and holds the blade beam in alignment, and its rigidity is the foundation of shearing accuracy: a frame that deflects during the cut lets the blade travel out of a straight line, and the plate edge comes off out of square. The guide surfaces along which the blade beam travels are machined so that the beam runs true through its stroke.
The blade beam and the upper blade. The blade beam is the moving member that carries the upper blade. The blade is a long straight rectangular section of tool steel, hardened and ground, with more than one usable cutting edge so that a dulled edge can be turned or reversed before the blade is finally reground. It is clamped along the beam so that it is supported over its full length, and its seating faces are machined so the blade is held straight.
The lower blade and the bed. The lower blade is set into the bed and forms the fixed cutting edge. The bed carries the plate through the cut and, together with the lower blade, establishes the reference face against which the plate is positioned and cut square.
The hold-down assembly. A row of hold-downs immediately beside the cutting line clamps the plate down onto the bed before and during the stroke. The hold-downs are the reason the plate is sheared rather than pushed, and they are the reason the cut edge comes off perpendicular to the plate face. Clamping force is a build characteristic of the machine and is specified for the plate range the machine is built to cut.
Blade gap adjustment. The clearance between the upper and lower blades is set to suit the material so that the plate is sheared cleanly rather than torn. It is adjustable, which is what allows the machine to cut a range of plate thicknesses as normal work rather than being set for one thickness.
Cutting angle adjustment. The angle at which the blade descends into the plate is adjustable. A larger angle lowers the peak cutting force required; a smaller angle produces a cleaner edge with more force needed. Adjustability allows the machine to be set for the thickness and the material being cut instead of being fixed by gearing.
The hydraulic power unit. Cylinders acting on the blade beam, a pump station with its motor, the valve arrangement controlling the cutting stroke and the return, and an oil reservoir. The hydraulic components are standard-specification items, so that seals, valves and pumps can be sourced and serviced locally or from the manufacturer.
The back gauge. The stop that positions the plate at the required cut length. It is carried on a mechanism travelling the length of the machine, guided so that it stays parallel to the blade along that travel, and it retracts after the cut so the cut blank clears the blade. The gauge can be set by hand, motorised and set from the control panel, or programmable with stored dimensions or sequences of dimensions.
Support and handling. Support arrangements at the entry side and the run-out side carry the plate at the correct height along its whole length before, during and after the cut. Support arms, roller supports and ball-transfer supports let heavy and long plate be moved into position and taken away without being lifted clear of the machine, and they keep the ends of the plate from hanging unsupported while it is being positioned against the back gauge.
The electrical control system. The machine is operated from a control panel which runs the cutting stroke, sets the back gauge dimension where a settable gauge is fitted, and sets the blade gap and cutting angle where these are powered. The panel, the foot switch that initiates the stroke, the motor starter and protection, and the safety devices — blade path guards and emergency stop — make up the electrical arrangement, built for the electrical supply of the destination site.
The conditions the machine works in — Saudi Arabia.
A shearing machine is not a machine whose specification is finished by its cutting capacity. It is installed in a workshop, in a climate, and it works for years in that environment. The Saudi Arabia conditions that matter to a plate shear are specific, and they are worth describing plainly because they shape how the machine is configured and how it is kept working.
High ambient temperature and sustained heat. Inland Saudi Arabia runs at high ambient temperatures through the working day for much of the year, and workshops of steel plate construction hold that heat. A hydraulic shearing machine develops heat in its own right as oil is pumped through the valve arrangement under load, and the workshop temperature adds to it. High oil temperature thins the oil, and thin oil affects a shearing machine in ways that show up as performance and as wear: the cutting stroke becomes less consistent, seals and valve components wear faster, and the machine’s settings have to be corrected more often. Machines built for this market are therefore configured with attention to the hydraulic system and to how the machine sheds heat, and the oil temperature and its behaviour through a working day are part of keeping the machine accurate rather than an afterthought.
Wind-blown dust and sand. Dust that gets into a machine does not announce itself. It works into the guiding surfaces along which the blade beam travels, into the back gauge mechanism, into the electrical panel and into the hydraulic breather, and its effect is progressive rather than immediate: the blade beam begins to run less freely, the back gauge becomes harder to set and less repeatable, and the hydraulic oil is contaminated over time. A machine for this environment is built with attention to how its moving surfaces, its gauge mechanism and its control arrangement are protected, and with the understanding that dust protection is a working requirement rather than a detail.
Coastal humidity and salt air. Saudi Arabia’s industrial activity is heavily concentrated on its coasts, where the air carries salt. Salt air attacks what it reaches: unpainted or thinly protected steel on the frame, the exposed surfaces of the blade zone, unpainted metal on the support arrangements, and the electrical enclosures. This is the reason the protective finish on the machine matters, and it is a maintenance consideration in the machine’s life rather than only a purchase-time specification.
Wide temperature variation. The difference between a hot working day and a cool night is considerable, and metal that moves through that cycle repeatedly works its fastenings and its fits. On a shearing machine this is felt in blade clamping, in the blade gap setting and in the gauge mechanism, and it is one reason blade gap and blade condition are checked as routine practice rather than only at long intervals.
The practical consequence. In this environment a plate shearing machine is kept accurate by attention to four things: the condition and protection of the hydraulic oil, the cleanliness of the blade beam guiding surfaces and the gauge mechanism, the condition of the blade and the correctness of the gap setting, and the protection of the electrical arrangement. None of these are unusual requirements, and none of them are difficult. They are simply the requirements of this market, and a machine configured and maintained for them performs for a long working life in a Saudi fabrication shop.
Product features and advantages.
Heavy rigid frame. The welded steel frame with thick side plates resists deflection under the cutting load, so the blade runs straight and the plate edge comes off square. Rigidity is what keeps shearing accuracy stable over years of plate work.
Hydraulic drive with controlled cutting force. Oil pressure drives the blade through the cut, giving a steady stroke and allowing the cutting angle and the cutting force to be set for the material rather than fixed by gearing.
Long straight blade cutting the full width in one stroke. The plate is sheared along a straight line across the full width of the machine in a single stroke, producing a square edge and giving the lowest cost per cut of any plate cutting method.
Adjustable cutting angle. The blade angle is set to suit the plate thickness and material, balancing cutting force against distortion so that heavy plate and thinner work are both cut cleanly.
Adjustable blade gap. The clearance between the blades is set to the material so that the plate is sheared through its thickness instead of being torn or left with a curved edge.
Tool steel blade with multiple usable edges. The hardened and ground blade carries more than one cutting edge and can be turned or reversed when an edge dulls, extending its life before regrinding.
Powerful hold-down clamping. The hold-downs beside the cutting line clamp the plate flat and still through the stroke, which prevents the plate from creeping and keeps the cut edge perpendicular to the plate face.
Repeatable cut length. The back gauge, guided parallel to the blade along the machine, positions the plate at a repeatable dimension so successive blanks come off at the same length.
Choice of back gauge control. Hand-set, motorised and set from the control panel, or programmable with stored dimensions and sequences of dimensions.
Support for long and heavy plate. Entry-side and run-out supports carry the plate at the correct height along its length so that heavy plate can be positioned and removed without being manhandled, and does not hang unsupported at the ends.
Hydraulic and electrical arrangement suited to a hot, dusty climate. The machine is built with attention to the hydraulic system and to the protection of its moving surfaces, gauge mechanism and control arrangement for the conditions of this market.
Built for the destination electrical supply. The machine is configured for the voltage, frequency and phase of the site where it will be installed.
Manufacturer direct. The machine is built by the manufacturer and supplied direct, which allows the cutting length and the plate range to be produced to what a workshop actually needs, and allows technical questions to be answered by the people who build the machine.
Cutting performance and edge quality.
The machine shears steel plate along a straight line across its full width, and the cut edge is formed in a single stroke. Working capability depends on plate thickness and cutting length together: the machine cuts its full length in thinner plate and its heaviest plate over a shorter length. Cutting capacity is also related to the material, because higher-strength plate requires more force to shear than mild steel of the same thickness. The machine is therefore specified against the plate range it will actually be given, and it performs at its best when the blade gap and the cutting angle are set to that material.
Cut edge quality depends on three things, all of which are build characteristics and settings of the machine. The blade gap must suit the material, so that the plate is sheared rather than torn. The cutting angle must suit the thickness, so that the plate is not distorted as it is cut. And the plate must be held flat and still by the hold-downs, so that the sheared edge is perpendicular to the plate face. Set correctly, the machine produces plate blanks with clean square edges ready for forming, fitting and welding, and square enough to be assembled without trimming.
Materials this machine cuts.
Mild steel and structural steel plate. The reference material for the machine’s cutting capacity and the material of most general plate fabrication.
Higher-tensile and higher-strength plate. Cut at a reduced thickness for the same machine, because these materials require more cutting force than mild steel of equal thickness.
Stainless steel plate. Used in water, process, food-related and architectural plate work; cut at a reduced thickness and requiring attention to the gap and angle settings.
Duplex and corrosion-resistant plate. Used where corrosion resistance is the reason for the material, as in water and process plant fabrication.
Galvanised and coated plate. Cut with the gap set to suit the coating and the material thickness so that the coating is not unnecessarily disturbed along the cut edge.
Because cutting force rises with the strength of the material, the machine is configured to the material range a workshop cuts, and the capacity of a given machine is stated for the material it is intended to cut. Stating the material is part of stating the specification.
Applications — Saudi steel fabrication.
Oil, gas and petrochemical fabrication. Plate blanks for tanks, vessels, separators, skids and supporting structures in the fabrication yards that serve the energy and process industries.
Water and desalination plant fabrication. Stainless and corrosion-resistant plate blanks for water treatment, desalination and process equipment.
Structural steelwork and industrial buildings. Base plates, connection plates, gusset plates, stiffener plate and bracket plate for steel buildings, industrial sheds, warehouses and plant structures.
Pipe racks, platforms, stairways and access structures. Cut plate for walkways, handrail plate, tread plate and access steelwork.
Ductwork and heavier HVAC fabrication. Plate and heavier-gauge blanks for duct sections, plenums and equipment housings where the material runs thicker than light sheet metal.
Trailer, tanker, container and heavy vehicle bodies. Cut plate for chassis plate, body panels, reinforcement plate and structural sections.
Industrial equipment and machine bases. Plate blanks for equipment frames, bases, guards and fabricated machinery components.
Architectural and general metalwork. Plate blanks where the cut edge is visible, or where plate is fitted against other plate.
Maintenance, repair and re-fabrication. Replacement plate cut to match existing plant and structures — a substantial and continuing demand in established industrial areas.
Build quality.
The machine is built as a heavy fabricated structure rather than assembled from light components. The frame is welded from steel plate and sections, and the side plates and bed are built to carry the cutting load without deflection. The surfaces on which the blade beam travels are machined so that the beam is guided true through its stroke, and the blade seating faces are machined so that the blade is held straight and supported along its length. The hydraulic system is assembled from standard-specification components. The electrical system is wired and tested as a complete arrangement, and the machine is run and checked before shipment so that the cutting stroke, the blade gap setting, the back gauge travel and the safety devices are verified as a complete machine.
Service and support.
Machines are supplied with documentation covering the machine, including the operating manual, the electrical drawings and the hydraulic arrangement. Installation and commissioning are carried out with technicians attending site, and operator training is provided so that the machine is set correctly for each material and operated safely. Illustrated manuals and video guidance cover the settings used most often, including the blade gap and cutting angle settings and their relationship to the plate being cut, and the routine attention the machine needs in a hot and dusty workshop. Engineering support is available for technical questions through the working life of the machine, and spare parts are supplied, with the blades and the hydraulic components given particular attention.
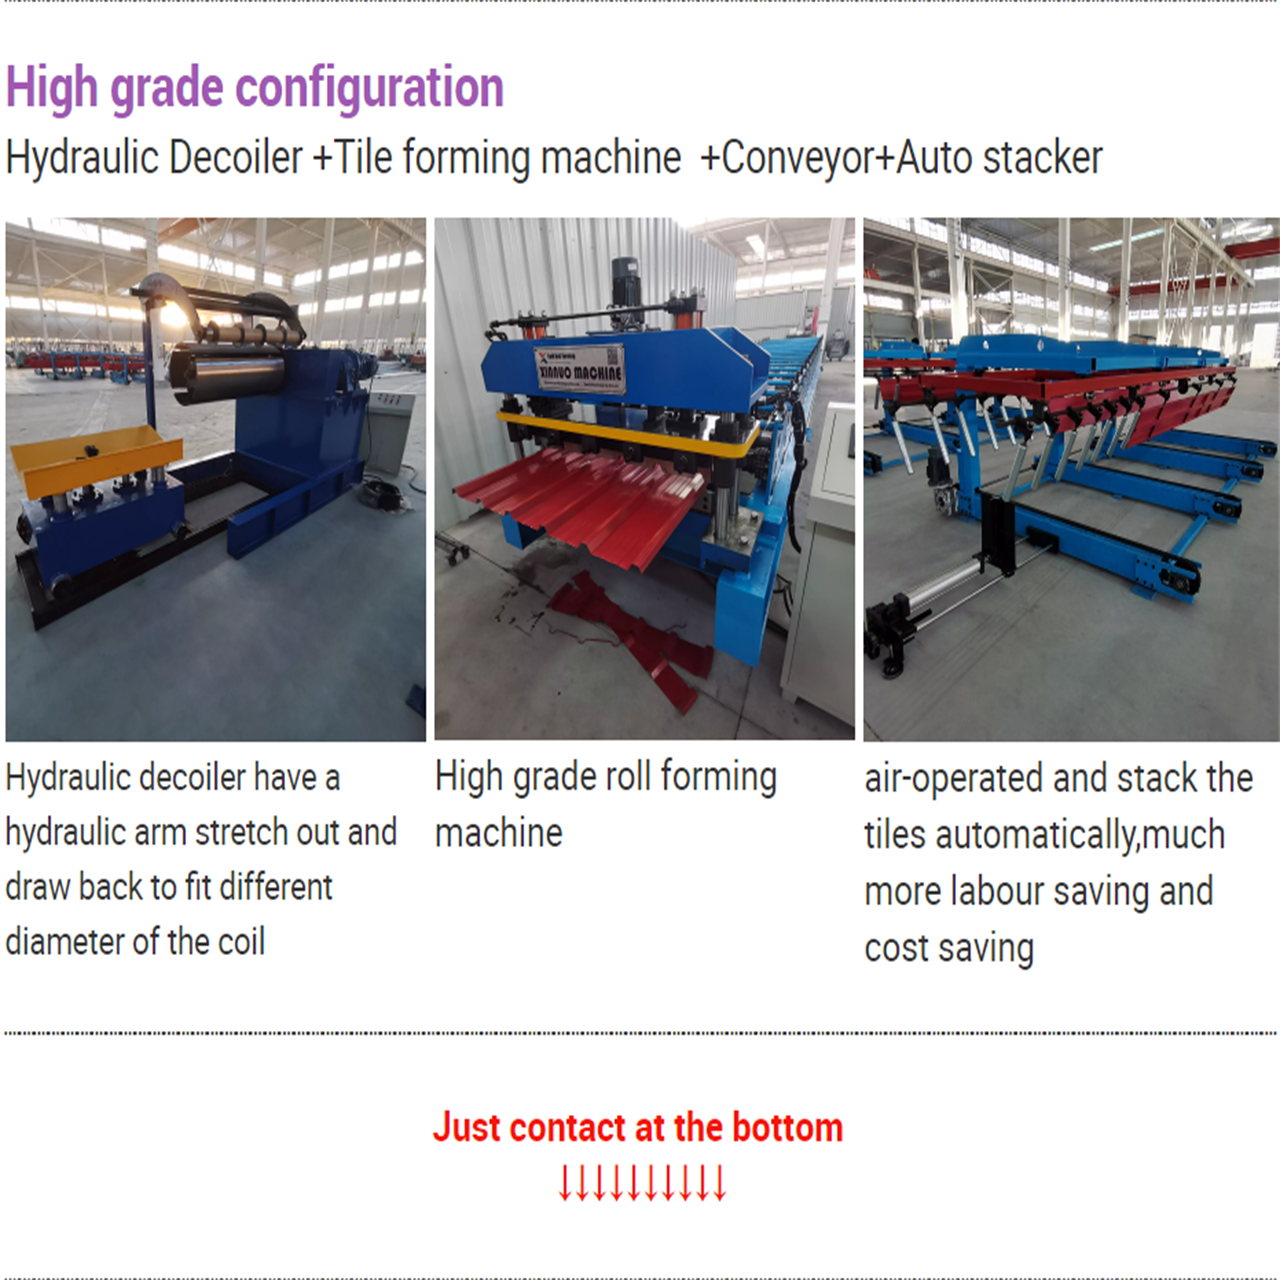
♦ COMPANY PROFILE:
Hebei Xinnuo Roll Forming Machine Co., Ltd., not only produce different types of professional roll forming machines, but also develop intelligent automatic roll forming production lines, C&Z shape purline machines, highway guardrail roll forming machine lines, sandwich panel production lines, decking forming machines, light keel machines, shutter slat door forming machines, downpipe machines, gutter machines, etc.
Advantages of Roll Forming A Metal Part
There are several advantages of using roll forming for your projects:
- The roll forming process allows operations such as punching, notching, and welding to be performed in-line. Labor cost and time for secondary operations are reduced or eliminated, reducing part costs.
- Roll form tooling allows for a high degree of flexibility. A single set of roll form tools will make almost any length of the same cross-section. Multiple sets of tools for varying length parts are not required.
- It can provide better dimensional control than other competing metal forming processes.
- Repeatability is inherent in the process, allowing easier assembly of roll formed parts into your finished product, and minimizing problems due to “standard” tolerance build up.
- Roll forming is typically a higher speed process.
- Roll forming offers customers a superior surface finish. This makes roll forming an excellent option for decorative stainless steel parts or for parts requiring a finish such as anodizing or powder coating. Also, texture or pattern can be rolled into the surface during forming.
- Roll forming utilizes material more efficiently than other competing processes.
- Roll formed shapes can be developed with thinner walls than competing processes
Roll forming is a continuous process which converts sheet metal into an engineered shape using consecutive sets of mated rolls, each of which makes only incremental changes in the form. The sum of these small changes in form is a complex profile.
-
Automatic Stacking & Palletizing Solutions...
-
XN cable tray making machine iron sheet making ...
-
Xinnnuo Round/Square Downpipe Cold Roll Forming...
-
sandwich panel product line sandwich hot press ...
-
Double layer Glazed Roof Tile roll forming mach...
-
Automatic double layer corrugated roof panel ro...