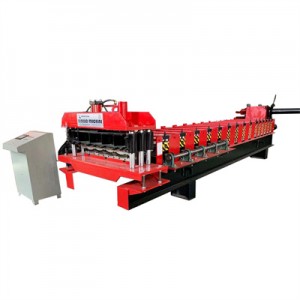
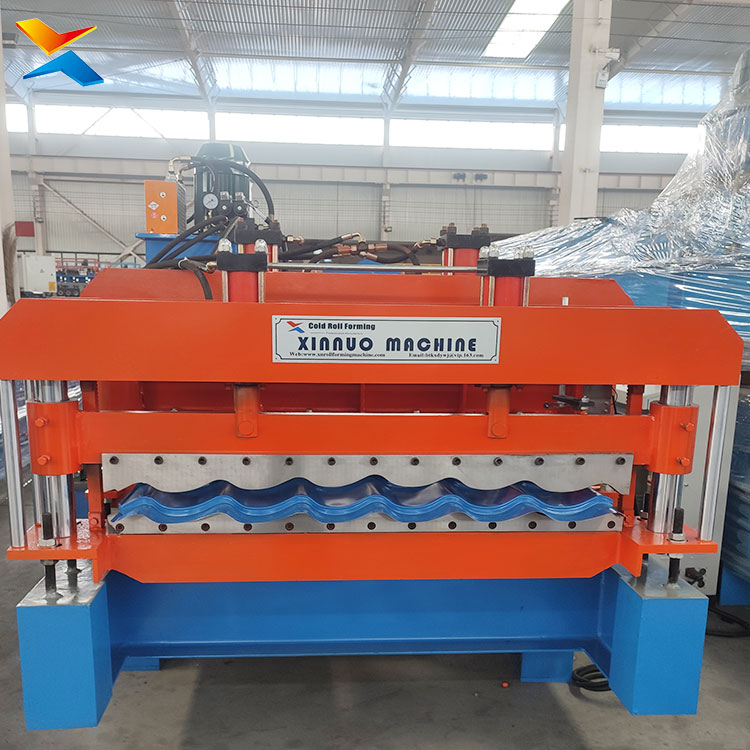
Metal roof tile machine and metal tile roof roll forming machine, supplied factory direct by the manufacturer to steel building projects in the Middle East. The machine forms coated steel coil into metal roof tile panels: panels that carry the curved, course-divided appearance of traditional roof tile, produced in steel so that a steel-framed building can wear a tiled roof without carrying tile.
A metal roof tile panel is not a metal roof sheet, and the difference decides the roof.
Both start as the same material and both end up covering a roof, so the two are often discussed as though one were a decorative version of the other. They are not the same component, and the difference does not lie in the surface pattern. It lies in how the panel carries load, how it is fixed, how a person walks on it, and what the building underneath has to provide.
A roof sheet is a covering that spans. It is produced in long lengths, it lands on purlins spaced to suit its own depth, it is fixed through the crest or with concealed clips, and it contributes to the diaphragm action of the roof. Its economy comes from length, few joints and light fixing.
A metal roof tile panel works on a different principle. Its depth is spent on the curve that gives the tile its shape rather than on a deep stiffening rib, so it spans a shorter distance and asks for closer support. Its coverage per panel is narrower, because a panel has to carry a countable number of tile courses across the slope. Its fixing is normally driven through the crest and then covered by the overlap of the next panel, so the finished roof shows no fastener. It is walked on in the pan, not on the crest, because a boot on the crest flattens the arc that the whole panel is for.
Those four differences are the reason a tiled steel roof is specified as a system rather than as a sheet. The purlin layout, the fixing schedule, the access plan and the repair method all follow the panel, and none of them can be decided after the panel is chosen.
What the panel asks of the building underneath.
Support at the spacing the panel’s stiffness allows. A tile panel’s depth is committed to appearance, so it does not have the spare depth of a structural roof sheet. The purlins come closer together, and the roof’s structure is designed around that layout rather than adjusted afterwards.
A fixing pattern that follows the crest. The fasteners are placed in the crest and then hidden by the following panel’s overlap. That placement is a property of the profile, not a site decision, and the number of fasteners per square metre is higher than on a wide sheet because each panel is narrower.
A pitch the profile can drain at. The arc that gives the tile its look also sets the minimum slope at which water leaves the roof rather than standing in the pans. A roof designed too shallow for the profile is a roof that will pond, and the profile cannot be asked to compensate.
Provision for movement. A metal panel expands and contracts with temperature across its length. On a roof in direct sun the movement is real, and the fixings and end details have to accommodate it rather than resist it.
Closure as matched components. The ridge, the hip, the verge, the eave and the change-of-slope detail are formed to the same profile as the panel. A ridge cap that is a generic bent strip will sit on top of the tile rather than seat into it, and that is where a tiled steel roof begins to leak.
The production route inside the machine.
The machine carries the coil through a sequence, and each stage leaves a permanent mark on the panel.
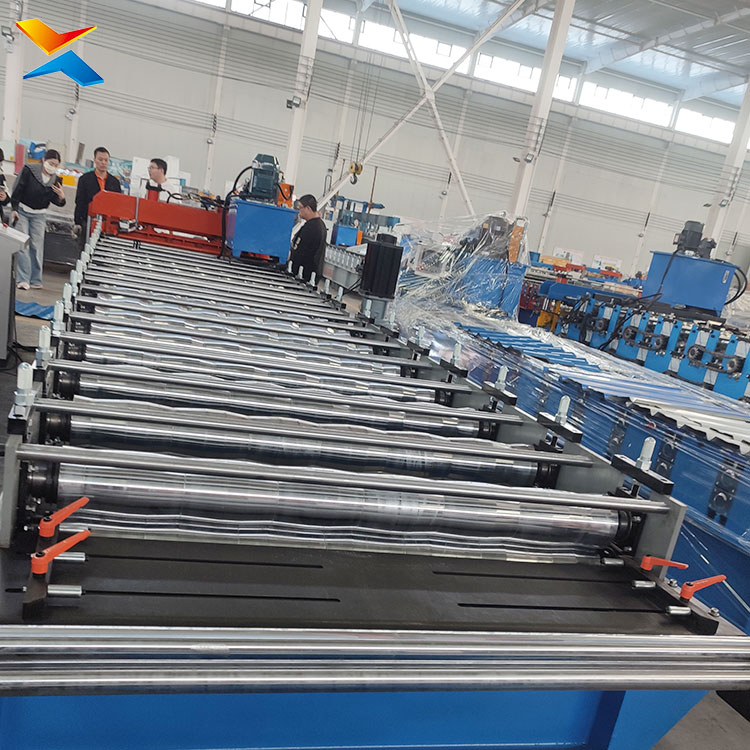
Entry and guidance. The coil is paid off, the strip is guided square to the machine and fed into the first stand. The alignment set here runs through every following stage, and a strip that enters skewed leaves the machine with an edge that wanders along its length.
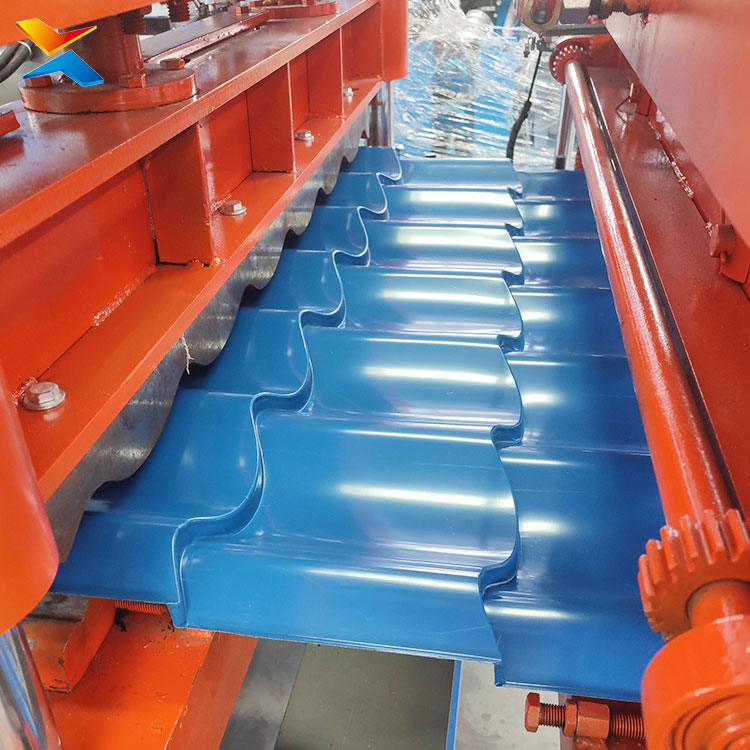
Arc forming. Pairs of rolls progressively turn the flat strip into the curve. The curve is not struck in one pass; it is accumulated across the stands, which is why the number of stands is a function of how deep the arc is.
Pitch stamping. The pitch device presses a division into the crest at each tile pitch, turning a continuous arc into a sequence of tile courses. This is the stage that makes the panel read as tile, and it is also the stage where a poorly controlled machine shows: the divisions are the one feature of the panel that is looked at directly, at close range, from the ground.
Edge forming. The side profiles are formed so that one panel laps into the next and the joint closes. The edge also determines how the panel terminates at a verge or a hip, which is why the edge profile and the accessory set have to come from the same drawing.
Cutting to length. The panel is cut after forming, at a position related to the pattern, so that a panel ends on a course line rather than in the middle of a tile. Cutting in the wrong place leaves a half tile at the eave that is visible on every panel of the roof.
Run-out. The finished panel leaves on a support that keeps it from being dragged or twisted as it comes off, because a panel that is handled badly after forming is a panel with a damaged arc.
The drive decides how regular the divisions are.
Two arrangements are built. In the standard arrangement the pitch device is driven from the machine’s main transmission through a chain or gear train, which ties its timing to the forming stands and keeps the machine simple. In the servo arrangement the pitch device is positioned by its own motor, with the forming drive carried through a bevel gearbox so that the two are controlled separately.
The difference is visible on the roof rather than on the drawing. A mechanically timed device holds its division spacing to whatever the chain and the gear train deliver, and that error accumulates along a long panel. A servo-positioned device holds each division to its own commanded position, so a panel run keeps the same course spacing from the first tile to the last, and a second panel run matches the first.
On a wall or a roof that is seen from the ground in raking light, the accumulated error is what a viewer notices first, because the eye reads the course lines as a regular grid and finds the one that is out. On a decorative roof, the regularity of the divisions is the product’s visible quality.
The profiles, and the tile idioms they answer.
The profiles fall into families, and the family is chosen by the roof the building is meant to have rather than by a rank of quality.
Fine pitch with closely spaced courses. A dense division pattern over a relatively shallow arc, reading as a finely worked tile surface. It suits restrained, detailed elevations and the smaller roof planes of residential work, where the roof is seen at a distance short enough for fine detail to register.
Medium pitch. The mainstream workhorse of the family: a division spacing and arc depth that read as a full-size classical tile without becoming heavy. It covers the widest range of villa and commercial work.
Broad pitch with a deep arc. Fewer, larger courses and a fuller curve, reading as a bold traditional tile. It suits wide roof planes and elevations where the roof is meant to be the dominant element.
Bamboo-joint profile. The deepest relief in the family, with the courses shaped to read as segmented bamboo-like joints. It is a decorative profile rather than a neutral one, and it belongs on buildings whose architecture is meant to be distinctive.
Asymmetric arc. The arc is formed unevenly so the panel reads as a three-dimensional tile rather than a symmetrical corrugation. It is the strongest reading of the family at close range.
Profiles carrying additional stiffening ribs. Extra ribs are pressed into the flat areas between courses, raising the panel’s stiffness without changing its tile reading. On wider purlin spacing or on a roof that will be walked for maintenance, this is the variant that keeps the panel’s shape.
Half-course edge profiles. The panel carries a half course at one or both edges, so that two panels laid side by side form one complete course across the joint. This is what allows a roof plane to be covered in whole panels and to finish at the verge on a course line rather than on a cut.
Materials and gauge.
The machine forms coated steel coil. The coil’s coating is the panel’s finish and its weather protection, and it is also the part that is tested hardest by the forming itself: a coating that cracks at the arc or at a course line exposes bare steel at exactly the place where the roof will begin to fail. The coating has to survive the forming, not merely arrive on the coil.
Gauge is a property of the profile and the drive rather than a free choice. A deep arc formed in thin strip will not hold its shape under a foot or a wind load, and a shallow arc formed in heavy strip loads the stands beyond what the profile was designed for. The gauge range belongs to the profile, and it is stated against the profile that will actually be run.
Configurations.
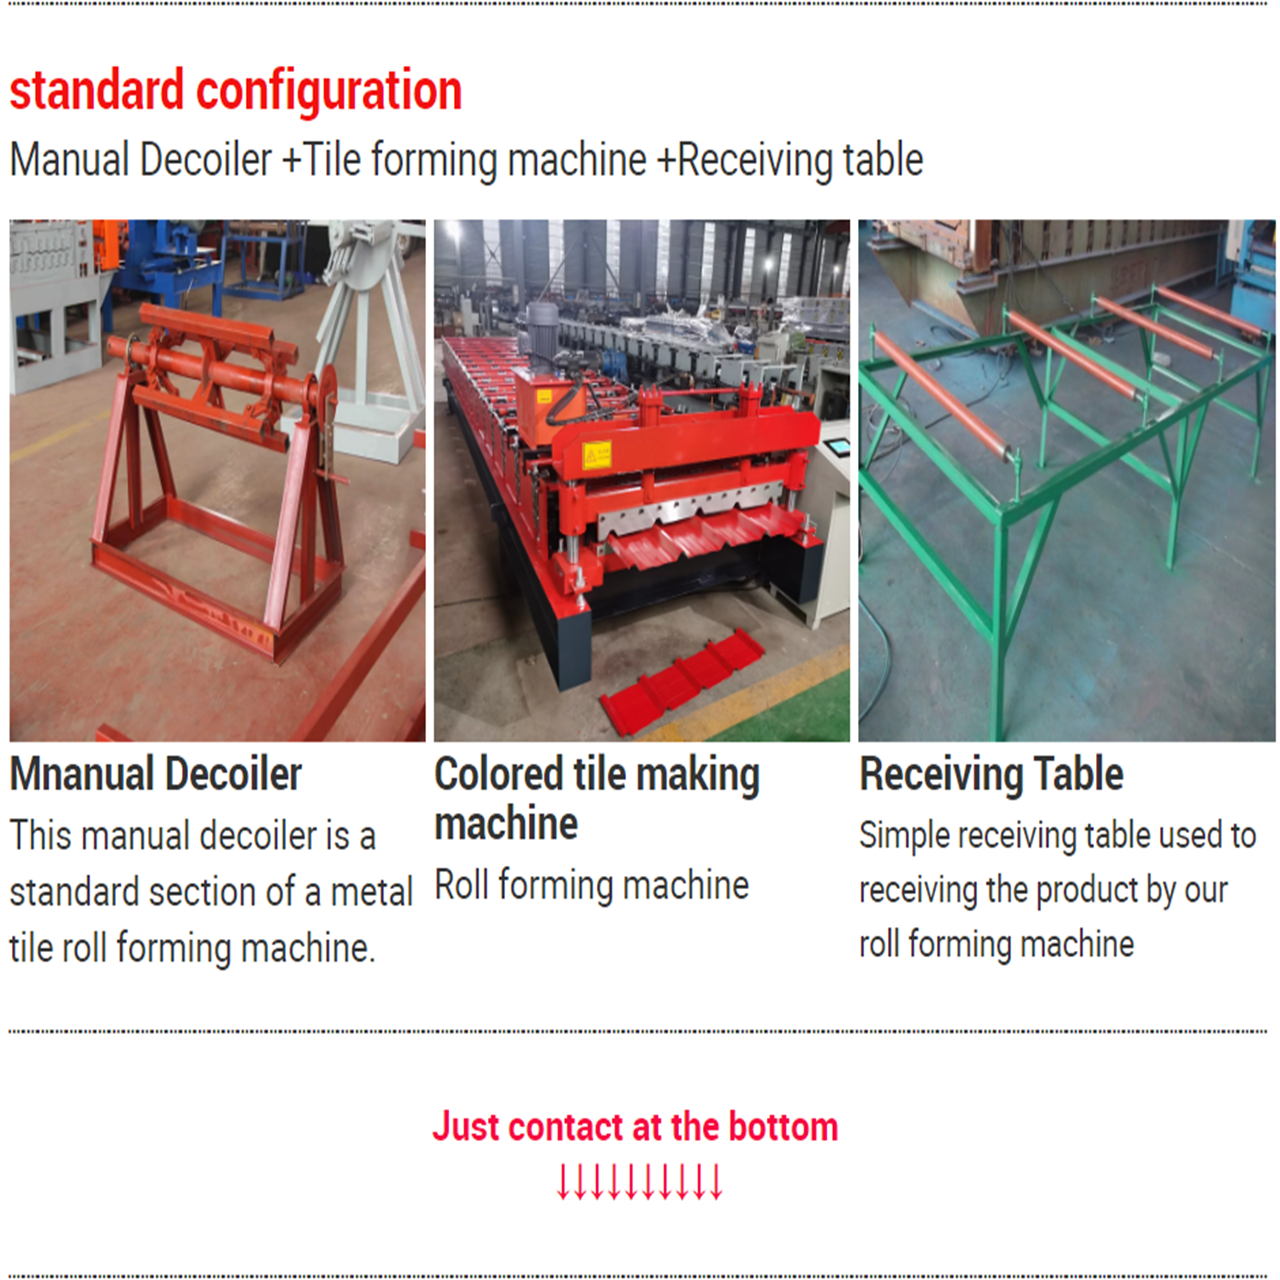
Standard single-profile machine. One set of tooling, one profile, one thickness range. The arrangement for a workshop that has settled on a single tile for its market.
Servo-driven pitch control. The pitch device positioned by its own motor, for the regularity described above.
Dual-width version. A machine that produces two panel widths by changing part of the tooling, for a workshop supplying roofs whose planes need different coverage.
Multi-material version. A machine configured so that coated steel and resin tile material can both be run, with the tooling changed between them. The two materials behave differently in forming, so the version is engineered for both rather than adapted from one.
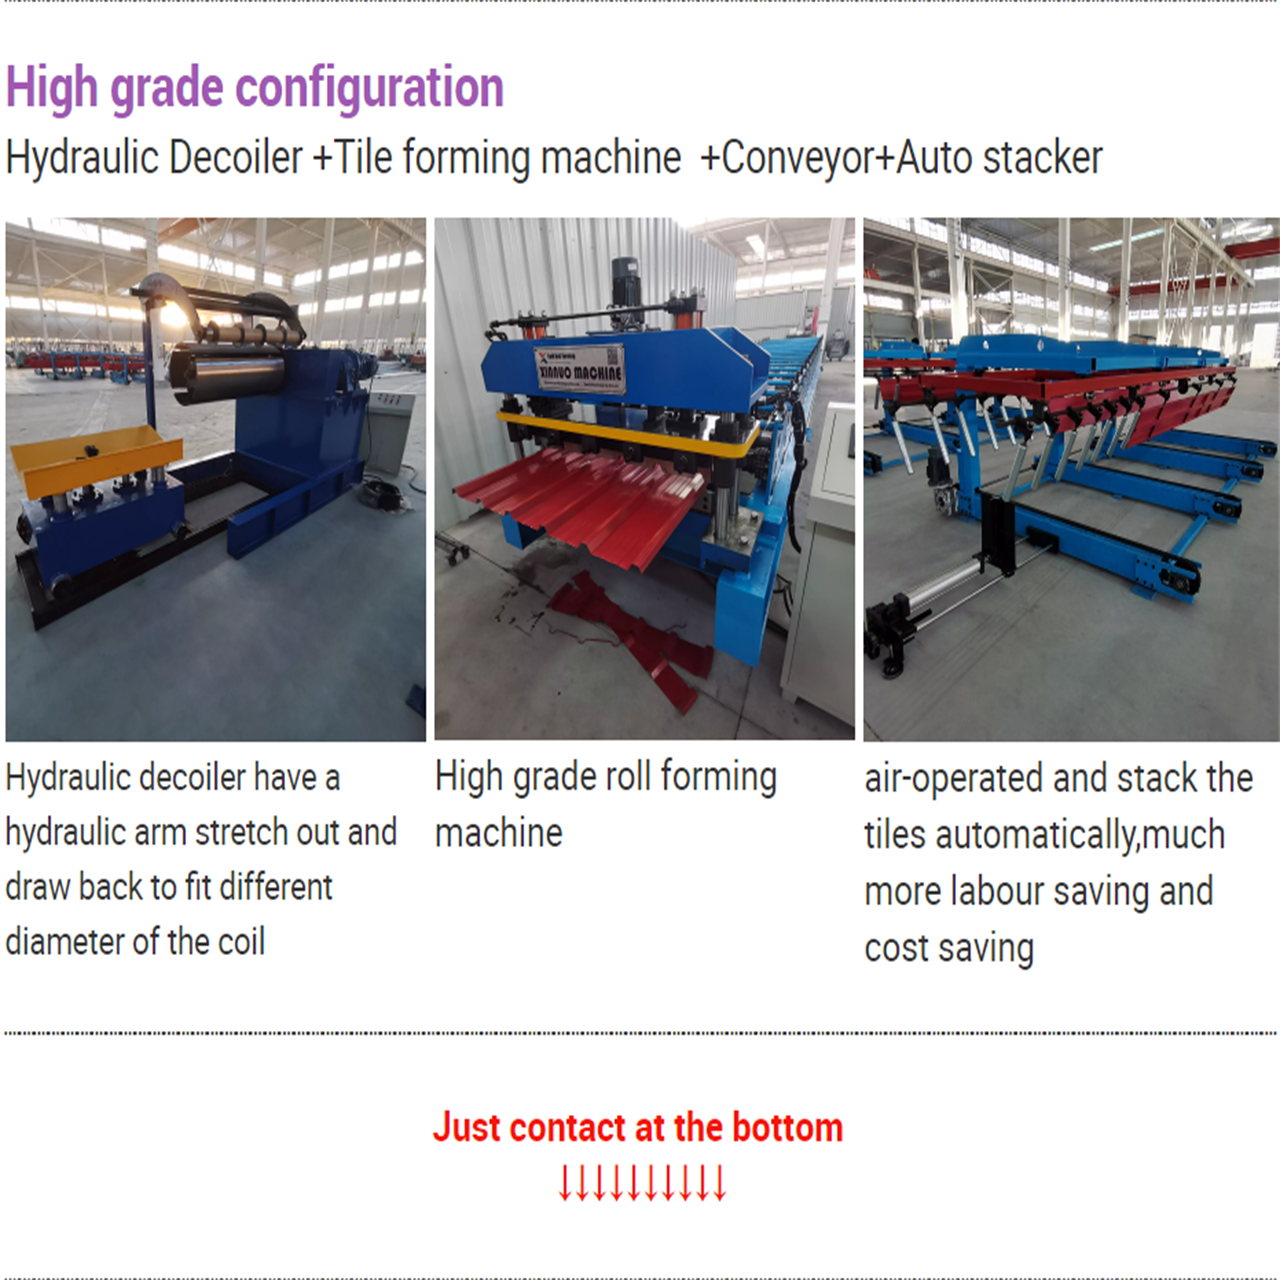
Higher-power builds. A heavier drive and frame for the deeper and wider profiles and for the higher line speeds, where the standard build’s motor and transmission would be the limit.
Machine build quality.
The frame is machined so that the upper and lower stands sit in line and hold their centres, because the arc is the sum of what every stand does and a frame that lets the stands drift produces a panel whose arc changes along its length. The forming rolls are made in pairs, hardened, ground and finished so that the working surface holds its shape in service. The shafts are alloy steel, ground, and sized to the load the profile puts on them. The pitch device’s tooling is a die set made for the pitch, not an adjustable approximation of it, which is why a pitch outside the archive means new tooling rather than a setting change. The structures are welded under shielding gas, stress-relieved where the design calls for it, shot-blasted, and finished with an electrostatic coating cured in an oven.
Product features and advantages.
Formed to the drawing rather than to a stock size. The panel is produced to the project’s profile, pitch, panel width, lengths and material, so the roof the building was designed with is the roof the machine is set to.
Two rhythms on one line. Arc forming and pitch stamping are separate functions on the same machine, so a change of tile reading is a change of pitch tooling rather than a change of machine.
A pitch device built as a die set. Each pitch in the archive has its own designed tooling, which is what holds the course spacing and the depth of the division to the same standard across a production run.
Fixed at the crest, hidden by the lap. The profile is formed so that the fastener sits in the crest and is covered by the following panel, leaving a finished roof with no exposed fixing.
A half-course edge for whole-panel coverage. The edge profile lets two panels form one complete course across the joint, so a roof plane is covered in whole panels and finishes on a course line.
Course-line cutting. The panel is cut relative to the pattern, so a panel ends on a course rather than through a tile.
Stiffening ribs where the roof will be walked. The ribbed variants raise the panel’s stiffness without changing its tile reading, for wider support spacing and for roofs maintained on foot.
Middle East conditions, in terms of the panel.
The panel is supplied into the Gulf markets — the United Arab Emirates, Saudi Arabia, Qatar, Oman, Kuwait and Bahrain — and the same panel meets two different exposures inside that group. The coastal cities of the Gulf, from the UAE’s shoreline through Saudi Arabia’s eastern province, work under humid, salt-bearing air for much of the year. The inland cities work under dry heat, hard sun and wind that carries sand. A project in either setting is served by the same machine, and the two settings load different parts of the panel.
Sun and heat. The panel runs at a temperature well above the air temperature, and it moves across its length accordingly. The fixing and the end details must let it move; a roof detailed as though the panel were static will either open at the laps or buckle in the pan. The coating carries the ultraviolet exposure, and the colour and gloss a roof holds over its life are a property of the coating rather than of the profile.
Dust and wind-blown sand. The course divisions that give the panel its tile appearance are also the places where dust settles and where a cleaning brush has to reach. A profile with deeper relief reads more strongly and holds more dust; the two go together and are chosen together on a dusty site.
Coastal salt air. The panel’s exposed cut edges, its fasteners and the ends of the laps are where corrosion begins, because those are the places where the coating is interrupted. A coated panel is a protected panel only while its coating is continuous, and every cut and every fixing is a break in it.
Rain that arrives in short intense events. The region’s rainfall is low in total but heavy when it comes. The roof has to clear a large volume in a short time, and the profile’s pans carry that water to the eave. A roof built too shallow for the profile, or with a blocked eave, ponds regardless of how little rain falls in the year.
Where the panel is used.
Villa roofs and villa compounds; mosque and religious buildings; hotel and resort roofs, including the pavilions, canopies and gate structures around them; showrooms and commercial frontages where the roof is part of the elevation; heritage-style and new-classical buildings that are steel-framed; entrance canopies, guard structures, gazebos and poolside buildings; and feature walls and screens where the same tile reading is carried down the façade.
Service and support.
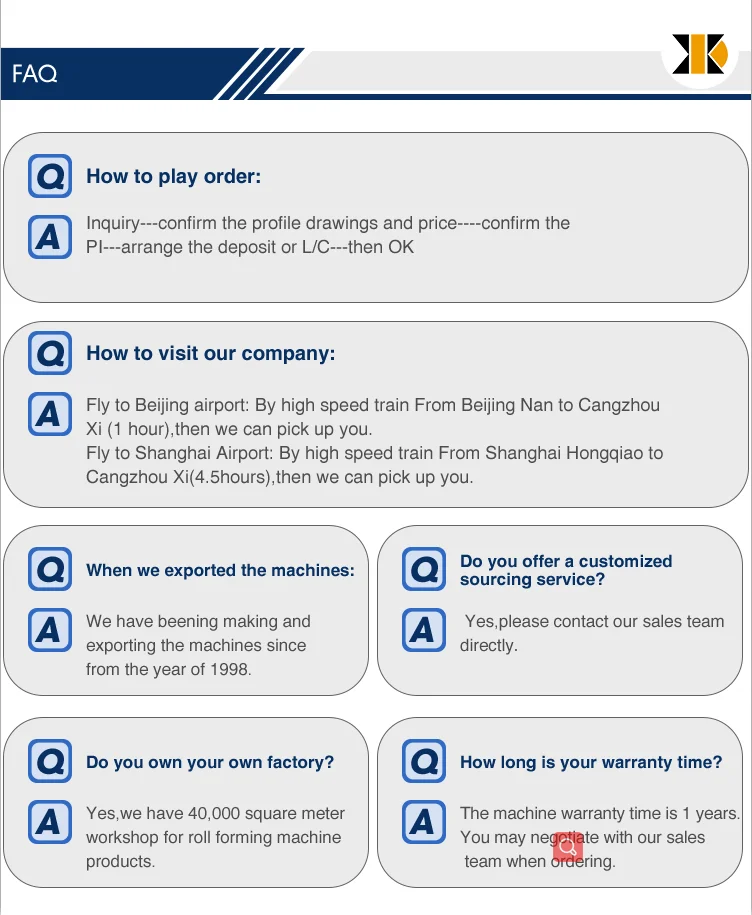
The machine is supplied with installation and commissioning support, operator training, illustrated manuals and a spare parts list, and with engineering support for the profile a project requires. Because the pitch tooling is specific to the pitch, the tooling record is part of what is handed over: it is what allows the same panel to be produced again for a later phase of the same project.
Factory direct.
The machine is built by the manufacturer and supplied directly, without a trading intermediary between the works and the buyer. The tooling comes out of the manufacturer’s own archive of glazed tile and arc profiles, which is why a profile already in that archive can be quoted against a drawing rather than developed from nothing.
♦ COMPANY PROFILE:
Hebei Xinnuo Roll Forming Machine Co., Ltd., not only produce different types of professional roll forming machines, but also develop intelligent automatic roll forming production lines, C&Z shape purline machines, highway guardrail roll forming machine lines, sandwich panel production lines, decking forming machines, light keel machines, shutter slat door forming machines, downpipe machines, gutter machines, etc.
There are several advantages of using roll forming for your projects:
- The roll forming process allows operations such as punching, notching, and welding to be performed in-line. Labor cost and time for secondary operations are reduced or eliminated, reducing part costs.
- Roll form tooling allows for a high degree of flexibility. A single set of roll form tools will make almost any length of the same cross-section. Multiple sets of tools for varying length parts are not required.
- It can provide better dimensional control than other competing metal forming processes.
- Repeatability is inherent in the process, allowing easier assembly of roll formed parts into your finished product, and minimizing problems due to “standard” tolerance build up.
- Roll forming is typically a higher speed process.
- Roll forming offers customers a superior surface finish. This makes roll forming an excellent option for decorative stainless steel parts or for parts requiring a finish such as anodizing or powder coating. Also, texture or pattern can be rolled into the surface during forming.
- Roll forming utilizes material more efficiently than other competing processes.
- Roll formed shapes can be developed with thinner walls than competing processes
In modern construction and manufacturing, the roll forming machine (commonly known as a roof tile or sheet metal roll former) has revolutionized profile fabrication. By replacing labor-intensive traditional press brake methods, advanced roll forming technology offers unmatched efficiency, quality, and cost savings for metal roofing and wall panel production.
Here are the key advantages of implementing a modern roll forming machine in your operations:
1. Unmatched High Efficiency and Output Speed
High-speed roll forming lines operate continuously, producing custom metal panels at speeds up to 20–40 meters per minute. This automated process significantly shortens lead times and accelerates project delivery cycles.
2. High Precision and Consistent Quality
Engineered with heavy-duty steel frames, high-precision roller dies, and PLC automated control systems, roll formers deliver pinpoint dimensional accuracy. Every panel exhibits uniform thickness, sharp profiles, and precise hole punching, ensuring seamless job-site installation.
3. Material Efficiency and Reduced Waste
Continuous roll forming minimizes scrap metal generation compared to conventional stamping. Precise coil feeding and automated hydraulic flying shears ensure optimal material utilization and reduced raw material costs.
4. Low Maintenance and Extended Durability
Constructed with heat-treated chrome-plated rollers and robust drive systems, industrial roll forming machines require minimal downtime while delivering a long service life under heavy daily operation.
Conclusion
Investing in a reliable roll forming machine boosts productivity, lowers labor costs, and guarantees consistent product quality—delivering maximum long-term return on investment (ROI) for metal fabrication businesses.
Metal roll forming is a continuous, automated metal fabrication process used to shape long strips of sheet metal (usually coiled steel or aluminum) into specific, uniform cross-sectional profiles.
Unlike traditional metal bending techniques like press braking—which shapes sheets batch by batch—roll forming operates as a continuous production line, making it one of the most efficient manufacturing methods for structural profiles, roofing panels, and automotive components.
How the Metal Roll Forming Process Works
The process passes coil stock through a series of consecutive roller dies to incrementally shape the metal into a finished cross-section:
-
Uncoiling: A heavy coil of sheet metal (often pre-painted, galvanized, or stainless steel) is mounted onto a decoiler and fed continuously into the line.
-
Progressive Forming: The strip passes through a sequence of mating roller stations (known as flower patterns). Each set of rollers gradually bends the metal by a few degrees. By making incremental bends, the process avoids overstressing the material or cracking protective coatings.
-
In-Line Processing (Optional): Pre-punching, post-punching, slitting, or embossing can be integrated directly into the automated line before or after forming.
-
Cutting to Length: Once the final profile is shaped, an automated flying shear or hydraulic cutter cuts the continuous panel into precise custom lengths without interrupting the line speed.
Key Advantages of Metal Roll Forming
-
Continuous High Output: Roll forming lines operate at high speeds (typically 20–50 meters per minute), significantly outperforming press brakes for mass production.
-
Tight Dimensional Tolerances: Advanced PLC automation and precision-machined rollers ensure strict dimensional consistency across every piece produced.
-
Material & Cost Efficiency: Minimizes scrap metal waste and eliminates extra handling steps by integrating punching, bending, and cutting into a single automated line.
-
Design Flexibility & Surface Protection: Capable of producing complex, multi-bend profiles while preserving surface finishes, galvanization, and paint coats.
Common Applications
Metal roll forming is widely used across multiple heavy-duty industries:
| Industry | Common Roll-Formed Products |
| Building & Construction | Trapezoidal roof tiles, standing seam panels, C/Z purlins, drywall studs, rain gutters |
| **Automotive &# What is Metal Roll Forming? |
Metal roll forming is a continuous, high-volume manufacturing process that bends long strips of sheet metal—usually coiled steel or aluminum—into custom cross-sectional profiles.
Unlike traditional press braking or stamping, which processes metal in single discrete batches, roll forming shapes metal incrementally at room temperature (cold forming) through a series of consecutive roller dies.
How Metal Roll Forming Works
The roll forming process relies on a line of paired roller stations that gradually shape the metal in steps:
-
Coil Unloading & Uncoiling: A heavy coil of flat metal strip is loaded onto an uncoiler and fed continuously into the machine.
-
In-Line Pre-Punching: Automatic presses notch, punch holes, or create slots in the flat strip prior to shaping.
-
Progressive Roll Shaping: The strip passes through multiple sets of upper and lower rollers (called roll stations). Each station bends the metal slightly more than the previous one, preventing stress fractures and material strain.
-
Cutting & Shearing: A flying hydraulic shear cuts the finished profile to exact target lengths without stopping the continuous line.
Key Benefits of Roll Forming
-
High Speed & Efficiency: Lines operate at speeds up to 20–50 meters per minute with minimal manual labor required.
-
Consistent Quality & Precision: Heavy-duty tool steel rollers controlled by PLC automation ensure exact tolerances across thousands of identical panels.
-
Material Waste Reduction: Continuous coil processing generates virtually zero scrap compared to conventional sheet stamping or trimming.
-
Complex Profiles: Produces intricate shapes—such as standing seam panels, hat channels, C/Z purlins, and tubular sections—in a single continuous pass.
Common Applications
-
Building & Construction: Roof tiles, wall cladding panels, gutters, structural purlins, and steel framing studs.
-
Automotive: Bumper beams, door impact bars, and chassis structural rails.
-
Solar & Energy: Solar panel mounting racks and support structures.
-
Storage & Industrial: Warehouse racking systems, shelving, and heavy-duty tracks.