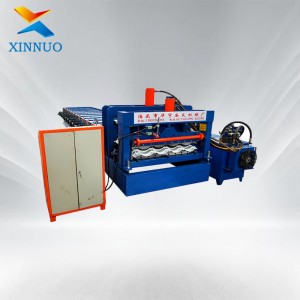


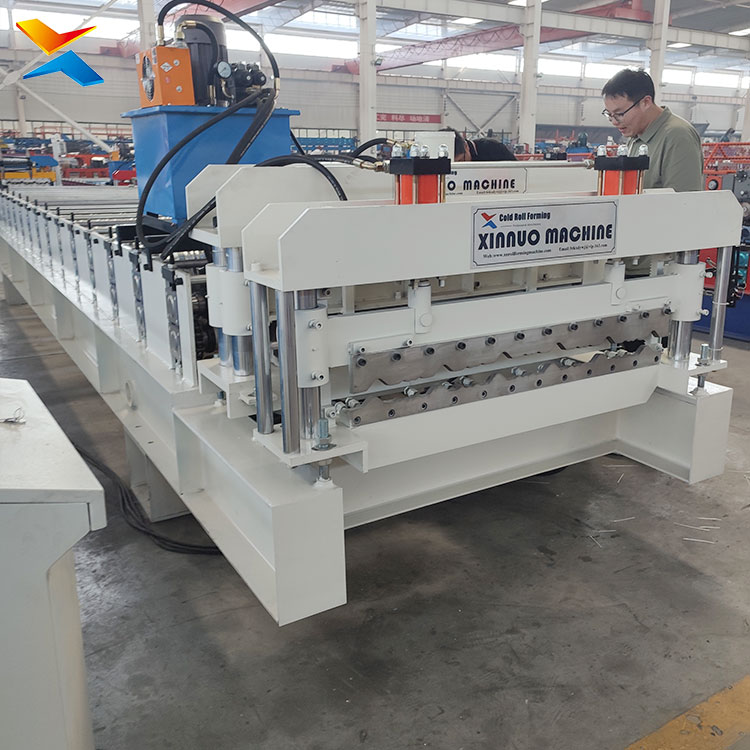
Double layer glazed tile roll forming machine — one machine body carrying two profiles, one of them a glazed tile roof panel. The machine stacks two independent sets of forming rollers one above the other inside a single frame, driven from one shared transmission system.
By repositioning the guide plates and baffles that lead the coil into the machine, the operator sends the strip into the upper roller set or the lower roller set, and the same body then produces either of the two profiles. In this family one of those two layers is a glazed tile layer: an arc-forming layer with an additional pitch-stamping device that presses an imprint across the peaks, so the finished panel reads as rows of antique roof tile rather than as a smooth continuous wave.
One profile at a time — the fact that defines the machine.
A double layer machine carries two tooling sets, not two production lines. Only one layer is active at a time, and the transmission drives whichever layer the strip has been guided into. There is no arrangement by which a single drive produces both profiles simultaneously.
The changeover is a guided one: the strip path is re-set into the other layer, and it is a procedure an operator learns and performs in a few minutes rather than a mechanical conversion. That is the machine’s working rhythm — one profile in a production run, then a changeover, then the other profile.
This shapes what the machine is for. It suits a workshop that needs two profiles but runs them in sequence: a product range in which both panels are sold, with demand for one following the other, or with batches large enough that a changeover is a reasonable cost against the saving of a second machine and a second footprint. Where two profiles genuinely have to run in parallel at volume, two single-layer machines are the correct arrangement, and the double layer arrangement is not a substitute for them.
What the double layer arrangement gives.
Two profiles from one footprint. The two roller stacks occupy the height of one machine body rather than the floor area of two. For a workshop where floor space is committed — and in the UAE that is usually the case — this is the arrangement’s main commercial purpose.
Two profiles from one drive. The forming drive is shared, so the machine carries one motor, one control arrangement and one set of switchgear rather than two.
One production position. One operator station, one infeed line and one outfeed arrangement serve both profiles.
A smaller investment than two machines. Because the frame, drive, control and infeed are shared, the double layer arrangement costs less than the two single-layer machines that would otherwise be needed for the same two profiles — which is the reason the arrangement exists.
A changeover rather than a second machine. Moving from one profile to the other is a re-setting of the strip path and the tooling, not the commissioning of another machine.
The glazed tile layer.
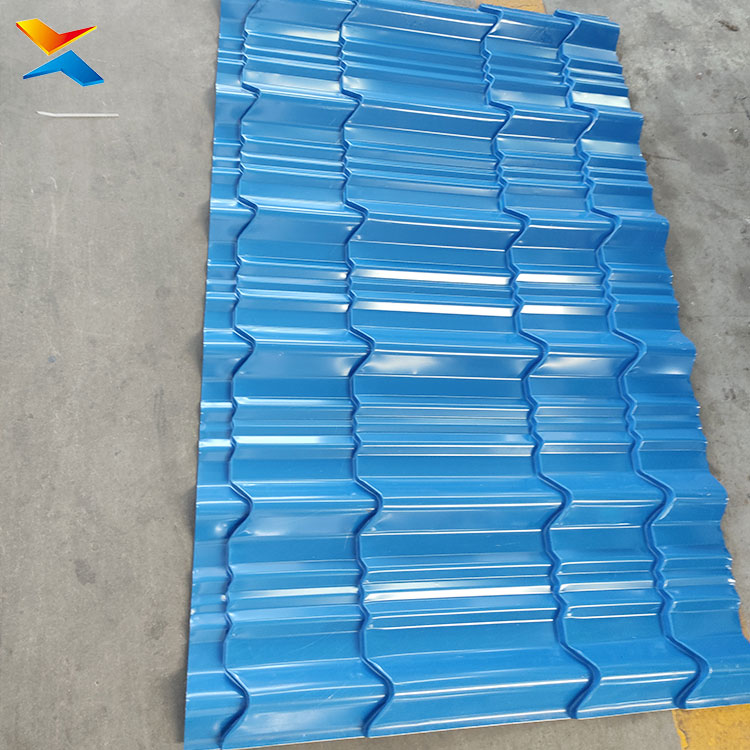
The glazed tile layer is an arc-forming layer. Roll forming brings the strip gradually into the arc of the tile across the full width of the panel, and the pitch-stamping device presses a division across the panel at each tile pitch, so the arc is divided along its length into tile courses.
What the layer produces is a metal panel with the appearance of antique roof tile. It is not ceramic, clay or resin — no machine in this family forms those materials — and the appearance is produced by the profile together with the tile divisions, while the panel’s colour and protection come from the coating system of the coil it is formed from.
The pitch is a dedicated stamping die rather than a setting. Where the pitch a buyer needs is already in the factory’s tooling archive, the machine is built on established tooling; where it is not, the die is designed and made for that pitch, which is a separate engineering step affecting both cost and schedule.
The combinations this machine is built in.
The family is not one machine. It covers a set of combinations, and each combination is a different engineering job because the two layers bring different forming processes into one frame. The combinations recorded as production-proven are grouped by what the two layers are.
Trapezoidal plus trapezoidal. Both layers are plain trapezoidal forming — the simplest combination, because both layers work by the same method, and the most economical in the family. Suited to a workshop that needs two trapezoidal profiles of different widths or peak counts, such as wall sheeting alongside roof sheeting.
Trapezoidal plus glazed tile. One layer forms a plain trapezoidal panel for structural roofing; the other forms glazed tile for decorative roofs. This is the most commonly ordered combination in the family, and it serves the customer who has to satisfy both ordinary and decorative demand from one machine. The glazed layer’s pitch stamping makes the changeover and commissioning more demanding than a two-trapezoid build.
Arc plus trapezoidal. One layer forms an arc-profile wave panel, the other a trapezoidal panel — the pairing that covers the two commonest roof panel types in one machine. This is the most exported combination in the family.
Arc plus glazed tile. One layer is a curved wave; the other is glazed tile. This is technically the most demanding of the common pairings, because the two layers belong to two different processes — continuous arc forming on one side, precise pitch stamping on the other — sharing one frame and one drive. It is the combination recorded for markets where antique-architecture demand and industrial building demand exist together, and the Middle East is named among those markets. On this build the chain specification has to satisfy the maximum torque demand of both layers together.
Arc plus arc. Both layers are arc wave profiles of differing wave height or wave pitch, for a customer needing two curved specifications.
Three-layer builds. Three roller sets stacked in one body. The most complex arrangement, engineered to order rather than selected, standing taller than a standard double layer machine and requiring a longer commissioning because all three tooling sets have to be aligned and set together.
Why the pairing decides the engineering.
Because each combination puts two different forming processes into one body, the pairing is not a matter of which two profiles a buyer happens to want. It decides the forming pass count the frame has to carry, the frame class, the chain specification, the drive arrangement on the glazed layer, and how long the machine takes to commission.
It also decides whether the two profiles can be produced on one body at all, which is the subject of the matching rules below.
Whether a pair of profiles belongs on one body.
Two profiles go on one double layer body only when the pair is matched, and the matching is checked in two places. Both checks come from the fact that the two layers share one frame and one drive.
Forming pass balance between the layers. The two layers should not differ greatly in forming pass count. Where one layer has considerably more passes than the other, the layer with more passes is formed fully while the layer with fewer can show profile defects, and because the two layers share one transmission they run at the same speed — so a large difference between the roll diameters of the two layers affects how smoothly the material runs. The smallest practical difference between the two layers is best; a moderate difference is workable; a large difference is handled by giving the slower layer more motor power or by adjusting the chain ratio; and a very large difference calls for engineering assessment rather than an order.
Feed width match between the layers. The best arrangement is for both layers to take the same feed width, because the two layers can then share one decoiler and one feed arrangement. Where the two widths differ by a small amount, guide blocks can be adjusted to accommodate both. Where the two widths differ substantially, the machine needs two guide systems and the changeover involves manually moving them, which is a heavier procedure than the guided changeover of a same-width machine.
Frame class from the heavier layer. The frame specification follows the heavier of the two layers, and because a double layer body carries both roller stacks and absorbs the vibration of both, it steps up a grade from the frame the same profile would need on a single-layer machine. A double layer body quoted with single-layer frame or chain specifications is a lighter machine than the work requires.
Chain specification from the highest torque layer. The chain follows the layer with the greatest torque demand, and is generally one grade above what a single-layer machine for that profile would use. On an arc plus glazed tile build this means the chain has to serve the arc layer and the pitch-stamping layer together.
The drive on the glazed layer.
The glazed layer’s drive is a distinct specification decision rather than a variant of the same machine. A servo-driven arrangement positions the pitch with considerably greater precision than a clutch-based arrangement, and the difference matters more on a double layer body than on a single-layer machine, because the glazed layer is one of two profiles the machine has to justify and because pitch positioning that drifts shows in the finished panel as an irregular tile line.
Where the product is sold into villa, mosque, heritage or hospitality work — projects in which the tile line is part of the design rather than a covering — the pitch positioning is not a place where the specification should be reduced. The machine here is available with the glazed layer on a standard drive or on a servo arrangement, and the newer builds in the family use a helical gear reducer for improved efficiency and a quieter, longer-lived drive.
When both layers are glazed tile.
A build in which both layers are glazed tile is the most demanding combination in the family, and it is engineered to order rather than selected from the range.
The difficulty is that two pitch systems have to be controlled independently, because each layer stamps its own pitch and the two cannot be driven from one pitch arrangement. If both layers ran on standard drives, pitch error would accumulate more; the arrangement used here puts at least one layer on servo control, and the practical transmission solution is a shared main forming drive with an independent servo motor controlling one layer’s pitch. Setting two pitch dies together is also a longer commissioning job than setting one, requiring an experienced commissioning engineer.
The result is a machine for a workshop whose entire decorative range is tile and which wants both tile profiles from one body — a different proposition from the trapezoidal plus glazed tile build that most of this family’s orders are for.
Materials and thickness.
The machine forms coated steel coil — steel carrying a metallic coating and a paint system, which is what gives the panel its colour and its protection in service. The coating is asked to survive the forming as well as the weather: a coating that cracks at the arcs and divisions exposes bare steel exactly where a roof weathers first, and on a Gulf coast that is where the roof begins to fail.
The working thickness is confirmed for each layer separately rather than as one figure for the machine, because the two layers are different forming jobs — a glazed tile layer carrying the load of forming the arc and stamping the pitch is worked differently from a plain trapezoidal layer, and the thickness that forms cleanly on one is not automatically the thickness that forms cleanly on the other.
Coil width is matched to a strip the buyer can actually source locally. A machine whose feed width corresponds to no strip available in the market is a machine that will stand idle, which is why the feed width is settled against the buyer’s own coil purchasing rather than against a preferred figure.
Machine structure.
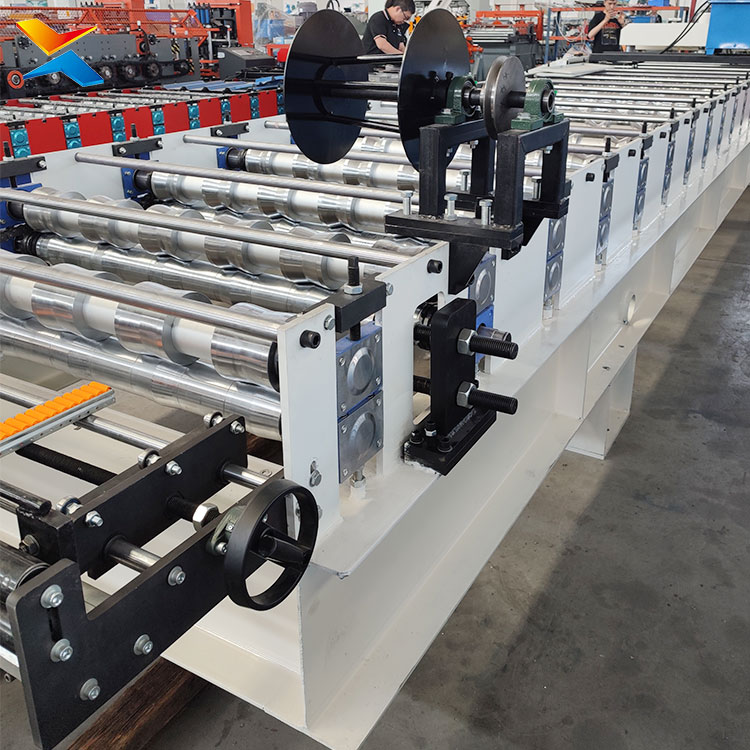
The frame. A heavy fabricated steel structure carrying both roller stacks and the glazed layer’s pitch device, machined so that every forming station in both layers measures from one flat reference. The frame class follows the heavier layer, and the machined reference is what allows two independent roller sets to be set up on one body at all.
The roller stacks. Two independent sets of forming stands and shafts, one above the other, each carrying its own profile’s tooling and each aligned to its own profile.
The shafts. Alloy steel, finish turned and externally ground for roundness and straightness under load.
The forming dies. Forged from carbon steel and carried through rough turning, hardening, finish turning, keyway cutting, polishing and electroplating, so that the working surface is hard, accurate and finished rather than merely shaped. Dies are made in matched pairs, because a profile is formed between two rolls.
The pitch-stamping device. Fitted to the glazed layer, with tooling made for that layer’s pitch and panel width.
The transmission. A shared main forming drive serving both layers, with the chain specification following the highest torque layer. On builds where one layer’s pitch is servo-controlled, that layer carries its own independent servo drive in addition to the shared main drive.
The cutting arrangement. The finished panel is cut to length within the production run, so a project’s roof is closed with panels made to the sizes it needs rather than cut down afterwards.
The control arrangement. The control sets the panel length, the run rate and the coordination of the forming stands, the pitch device and the cutting arrangement, and it is where the settings that recur in this kind of work are held — a new panel length, and setting up for the other layer.
The electrical arrangement. Wired and tested as a complete unit, and configured for the voltage, frequency and phase of the installation site.
The welding and the finish. Shielded welding, with surfaces shot blasted and then electrostatically sprayed and baked for protection.
Where this machine is used.
Structural roofing. The trapezoidal or arc layer produces the plain panel that covers the industrial and commercial buildings of a market — plants, warehouses, workshops, agricultural buildings and wide-span structures.
Decorative and traditional roofing. The glazed tile layer produces the panel for buildings whose architecture calls for a tiled roof — villas, mosques and religious buildings, hospitality and resort buildings, showrooms and commercial frontages, entrance and gate structures, and landscape and garden buildings.
A product range rather than one product. The machine’s main application is the workshop that has to serve both of those demands. This is why the trapezoidal plus glazed tile pairing is the most commonly ordered combination in the family: one machine covers ordinary structural demand and decorative demand, and the operator changes over between them as the order book requires.
Wall and façade work. Where a profile is suitable for walls, screens and soffits as well as roofs, the same machine covers those uses, which matters where a project wants its tile or wave reading carried across a whole building rather than only on its roof.
The machine in Middle East conditions.
The arc plus glazed tile combination — a curved wave panel on one layer and glazed tile on the other — is the pairing the factory’s records associate with markets where antique-architecture demand and industrial building demand exist side by side, and the Middle East is named among those markets. That pairing puts the two faces of the region’s building in one machine: the ordinary structural roof of the working building, and the tiled roof of the building that is meant to be seen.
Three conditions shape the machine’s service in the region, and all three put the emphasis on parts that the machine cannot substitute for.
Coastal humidity and salt-laden air. Along the Gulf coast the air carries salt, and the panel is exposed to it at every edge, fixing, cut and drilled hole. The panel field is protected by its coating, and corrosion begins at the details. The machine forms the geometry; the coating system chosen for the coil decides how long the appearance survives — so a durability question answered with a machine figure is an answer to a different question.
High ambient temperature and the machine’s own heat. The machine runs in high ambient temperature for long periods, and where the drive arrangement and the gear reducer generate their own heat, the oil thins and the machine’s cooling and lubrication routine carry more weight than they would in a temperate workshop. On a double layer body this is worth attention because there is more transmission in one frame, and because the two layers share it.
Wind-blown dust and sand. Dust settles into the glazed layer’s tile divisions and into the arc troughs, and it reaches the pitch-stamping device, the guide plates that set the strip path between the layers, the cutting arrangement and the control enclosure. On a double layer machine the guide plates and baffles are also the parts that define the changeover, so keeping them clean and correctly set is a maintenance task in this environment rather than an occasional one.
Intense rain in a short season. Rainfall in the region is concentrated and heavy when it comes, and the roof has to pass an intense event quickly. On a tile profile the water’s route off the plane follows the arcs and the divisions and the overlapping edges do the sealing, so the laps and the pitch relationship between them are set by the profile rather than by the installation.
The flat-roof reality. A large part of the region’s building is on flat roofs, and the decorative layer serves the projects whose design already calls for a tiled roof rather than converting a flat roof into one. The structural layer, by contrast, serves the region’s industrial and commercial building directly. A machine carrying both is therefore a machine for a workshop whose market includes both.
Workshop requirements.
A double layer machine is taller and heavier than the single-layer machine for either of its profiles, and a glazed tile layer adds tooling weight to that. The machine therefore needs clear height for the body itself and for lifting the upper roller set during commissioning and maintenance, a floor that carries the assembled weight, and an access route for the machine and for the lifting of its heaviest assemblies. It is a workshop-level requirement of the machine rather than an optional consideration.
Product features and advantages.
Two profiles from one footprint and one drive. Two roller stacks in one body, one motor, one control arrangement and one infeed line, rather than two machines.
A smaller investment than two single-layer machines. The frame, drive, control and infeed are shared, which is the commercial purpose of the arrangement.
A guided changeover. Moving between the two profiles is a re-setting of the strip path rather than a mechanical conversion or a second machine.
A glazed tile layer that carries the pitch-stamping device. The arc is formed and the tile division pressed in the same pass, so the panel leaves the machine reading as laid tile rather than as a smooth wave.
Forming, stamping and cutting in one pass. Panels are cut to length within the production run, so a roof or an elevation is closed with panels made to the sizes it needs.
A pair of profiles matched before the machine is built. The forming pass balance and the feed width match between the layers are checked as part of specifying the machine, and the frame and chain follow the heavier and the higher-torque layer respectively.
Frame and chain specified for the double layer body. The frame steps up from what the same profile would need on a single-layer machine, because it carries both stacks and absorbs both vibrations.
Servo pitch positioning available on the glazed layer. Where the tile line is part of the building’s design, the glazed layer can be supplied with servo control for pitch positioning rather than a clutch-based arrangement.
Both layers glazed tile available as an engineered build. For a workshop whose whole decorative range is tile, with independent pitch control and at least one layer on servo.
Independently confirmed thickness for each layer. Rather than one figure applied to a machine carrying two different forming jobs.
Three-layer and dual-width builds within the family. Where a workshop needs three profiles or two panel widths, the family covers those arrangements rather than requiring several machines.
A wider family of combination types. Trapezoidal plus trapezoidal, trapezoidal plus glazed tile, arc plus trapezoidal, arc plus glazed tile, arc plus arc and three-layer builds, so a workshop’s requirement is met by the appropriate pairing rather than the nearest one available.
Build quality. Dies forged, hardened, finish turned, polished and electroplated and made in matched pairs; shafts in alloy steel, ground for roundness and straightness under load; frames machined on CNC gantry mills so that every station in both layers measures from one flat reference; shielded welding with shot blasting and an electrostatically sprayed, baked finish.
Configured for the destination electrical supply. Voltage, frequency and phase of the installation site.
Factory direct, from a tooling archive. The machine is built and supplied by the manufacturer rather than resold, and it is built from a tooling archive rather than designed from scratch for each order, so the closest production-proven blueprint is identified for a buyer’s pair of profiles before tooling is committed.
Service and support.
Machines are supplied with documentation covering the machine, including the operating manual, the electrical drawings and the arrangement of the forming sequence for both layers, together with the profiles, pitches and panel widths the tooling was made for. Installation and commissioning are carried out with technicians attending site; commissioning a double layer machine is a longer job than commissioning a single-layer machine, because two tooling sets have to be aligned and set together and, on a glazed layer, the pitch device has to be set and verified. Operator training covers the changeover between the two layers, including the setting of the guide plates and baffles that direct the strip, the setting of panel lengths in the control, and the inspection of panels against the standard the product requires. Illustrated manuals and video guidance cover the settings adjusted most often, and the routine attention the machine needs where heat and dust are constant. Engineering support is available for technical questions through the working life of the machine, and spare parts are supplied, with the pitch-stamping tooling, the forming dies, the guide plates and the transmission components given particular attention.
How this machine is supplied.
The machine is supplied factory direct to the UAE and the wider region, configured for the installation site’s electrical supply and built to the buyer’s pair of profiles. Because the family is configured rather than stocked, the machine is specified from a buyer’s requirements rather than selected from a catalogue: the pairing and which layer carries the glazed profile, the two profiles with their peak counts, pitches and effective widths, the working thickness for each layer, the feed width each layer needs, the drive arrangement on the glazed layer, and the workshop’s clear height and lifting arrangements. From those the factory identifies the closest production-proven blueprint in the archive, checks whether the two profiles and the pitch match existing tooling or require new tooling, fixes the frame class and chain specification from the heavier and higher-torque layer, and supplies the machine with its layout drawing, documentation, commissioning and training scope, and spare parts list.
♦ COMPANY PROFILE:
Hebei Xinnuo Roll Forming Machine Co., Ltd., not only produce different types of professional roll forming machines, but also develop intelligent automatic roll forming production lines, C&Z shape purline machines, highway guardrail roll forming machine lines, sandwich panel production lines, decking forming machines, light keel machines, shutter slat door forming machines, downpipe machines, gutter machines, etc.
There are several advantages of using roll forming for your projects:
- The roll forming process allows operations such as punching, notching, and welding to be performed in-line. Labor cost and time for secondary operations are reduced or eliminated, reducing part costs.
- Roll form tooling allows for a high degree of flexibility. A single set of roll form tools will make almost any length of the same cross-section. Multiple sets of tools for varying length parts are not required.
- It can provide better dimensional control than other competing metal forming processes.
- Repeatability is inherent in the process, allowing easier assembly of roll formed parts into your finished product, and minimizing problems due to “standard” tolerance build up.
- Roll forming is typically a higher speed process.
- Roll forming offers customers a superior surface finish. This makes roll forming an excellent option for decorative stainless steel parts or for parts requiring a finish such as anodizing or powder coating. Also, texture or pattern can be rolled into the surface during forming.
- Roll forming utilizes material more efficiently than other competing processes.
- Roll formed shapes can be developed with thinner walls than competing processes
In modern construction and manufacturing, the roll forming machine (commonly known as a roof tile or sheet metal roll former) has revolutionized profile fabrication. By replacing labor-intensive traditional press brake methods, advanced roll forming technology offers unmatched efficiency, quality, and cost savings for metal roofing and wall panel production.
Here are the key advantages of implementing a modern roll forming machine in your operations:
1. Unmatched High Efficiency and Output Speed
High-speed roll forming lines operate continuously, producing custom metal panels at speeds up to 20–40 meters per minute. This automated process significantly shortens lead times and accelerates project delivery cycles.
2. High Precision and Consistent Quality
Engineered with heavy-duty steel frames, high-precision roller dies, and PLC automated control systems, roll formers deliver pinpoint dimensional accuracy. Every panel exhibits uniform thickness, sharp profiles, and precise hole punching, ensuring seamless job-site installation.
3. Material Efficiency and Reduced Waste
Continuous roll forming minimizes scrap metal generation compared to conventional stamping. Precise coil feeding and automated hydraulic flying shears ensure optimal material utilization and reduced raw material costs.
4. Low Maintenance and Extended Durability
Constructed with heat-treated chrome-plated rollers and robust drive systems, industrial roll forming machines require minimal downtime while delivering a long service life under heavy daily operation.
Conclusion
Investing in a reliable roll forming machine boosts productivity, lowers labor costs, and guarantees consistent product quality—delivering maximum long-term return on investment (ROI) for metal fabrication businesses.
Metal roll forming is a continuous, automated metal fabrication process used to shape long strips of sheet metal (usually coiled steel or aluminum) into specific, uniform cross-sectional profiles.
Unlike traditional metal bending techniques like press braking—which shapes sheets batch by batch—roll forming operates as a continuous production line, making it one of the most efficient manufacturing methods for structural profiles, roofing panels, and automotive components.
How the Metal Roll Forming Process Works
The process passes coil stock through a series of consecutive roller dies to incrementally shape the metal into a finished cross-section:
-
Uncoiling: A heavy coil of sheet metal (often pre-painted, galvanized, or stainless steel) is mounted onto a decoiler and fed continuously into the line.
-
Progressive Forming: The strip passes through a sequence of mating roller stations (known as flower patterns). Each set of rollers gradually bends the metal by a few degrees. By making incremental bends, the process avoids overstressing the material or cracking protective coatings.
-
In-Line Processing (Optional): Pre-punching, post-punching, slitting, or embossing can be integrated directly into the automated line before or after forming.
-
Cutting to Length: Once the final profile is shaped, an automated flying shear or hydraulic cutter cuts the continuous panel into precise custom lengths without interrupting the line speed.
Key Advantages of Metal Roll Forming
-
Continuous High Output: Roll forming lines operate at high speeds (typically 20–50 meters per minute), significantly outperforming press brakes for mass production.
-
Tight Dimensional Tolerances: Advanced PLC automation and precision-machined rollers ensure strict dimensional consistency across every piece produced.
-
Material & Cost Efficiency: Minimizes scrap metal waste and eliminates extra handling steps by integrating punching, bending, and cutting into a single automated line.
-
Design Flexibility & Surface Protection: Capable of producing complex, multi-bend profiles while preserving surface finishes, galvanization, and paint coats.
Common Applications
Metal roll forming is widely used across multiple heavy-duty industries:
| Industry | Common Roll-Formed Products |
| Building & Construction | Trapezoidal roof tiles, standing seam panels, C/Z purlins, drywall studs, rain gutters |
| **Automotive &# What is Metal Roll Forming? |
Metal roll forming is a continuous, high-volume manufacturing process that bends long strips of sheet metal—usually coiled steel or aluminum—into custom cross-sectional profiles.
Unlike traditional press braking or stamping, which processes metal in single discrete batches, roll forming shapes metal incrementally at room temperature (cold forming) through a series of consecutive roller dies.
How Metal Roll Forming Works
The roll forming process relies on a line of paired roller stations that gradually shape the metal in steps:
-
Coil Unloading & Uncoiling: A heavy coil of flat metal strip is loaded onto an uncoiler and fed continuously into the machine.
-
In-Line Pre-Punching: Automatic presses notch, punch holes, or create slots in the flat strip prior to shaping.
-
Progressive Roll Shaping: The strip passes through multiple sets of upper and lower rollers (called roll stations). Each station bends the metal slightly more than the previous one, preventing stress fractures and material strain.
-
Cutting & Shearing: A flying hydraulic shear cuts the finished profile to exact target lengths without stopping the continuous line.
Key Benefits of Roll Forming
-
High Speed & Efficiency: Lines operate at speeds up to 20–50 meters per minute with minimal manual labor required.
-
Consistent Quality & Precision: Heavy-duty tool steel rollers controlled by PLC automation ensure exact tolerances across thousands of identical panels.
-
Material Waste Reduction: Continuous coil processing generates virtually zero scrap compared to conventional sheet stamping or trimming.
-
Complex Profiles: Produces intricate shapes—such as standing seam panels, hat channels, C/Z purlins, and tubular sections—in a single continuous pass.
Common Applications
-
Building & Construction: Roof tiles, wall cladding panels, gutters, structural purlins, and steel framing studs.
-
Automotive: Bumper beams, door impact bars, and chassis structural rails.
-
Solar & Energy: Solar panel mounting racks and support structures.
-
Storage & Industrial: Warehouse racking systems, shelving, and heavy-duty tracks.