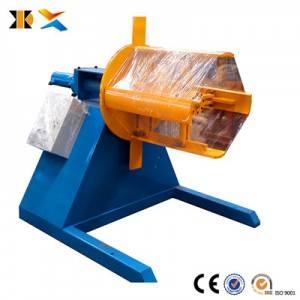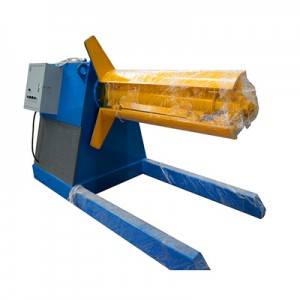
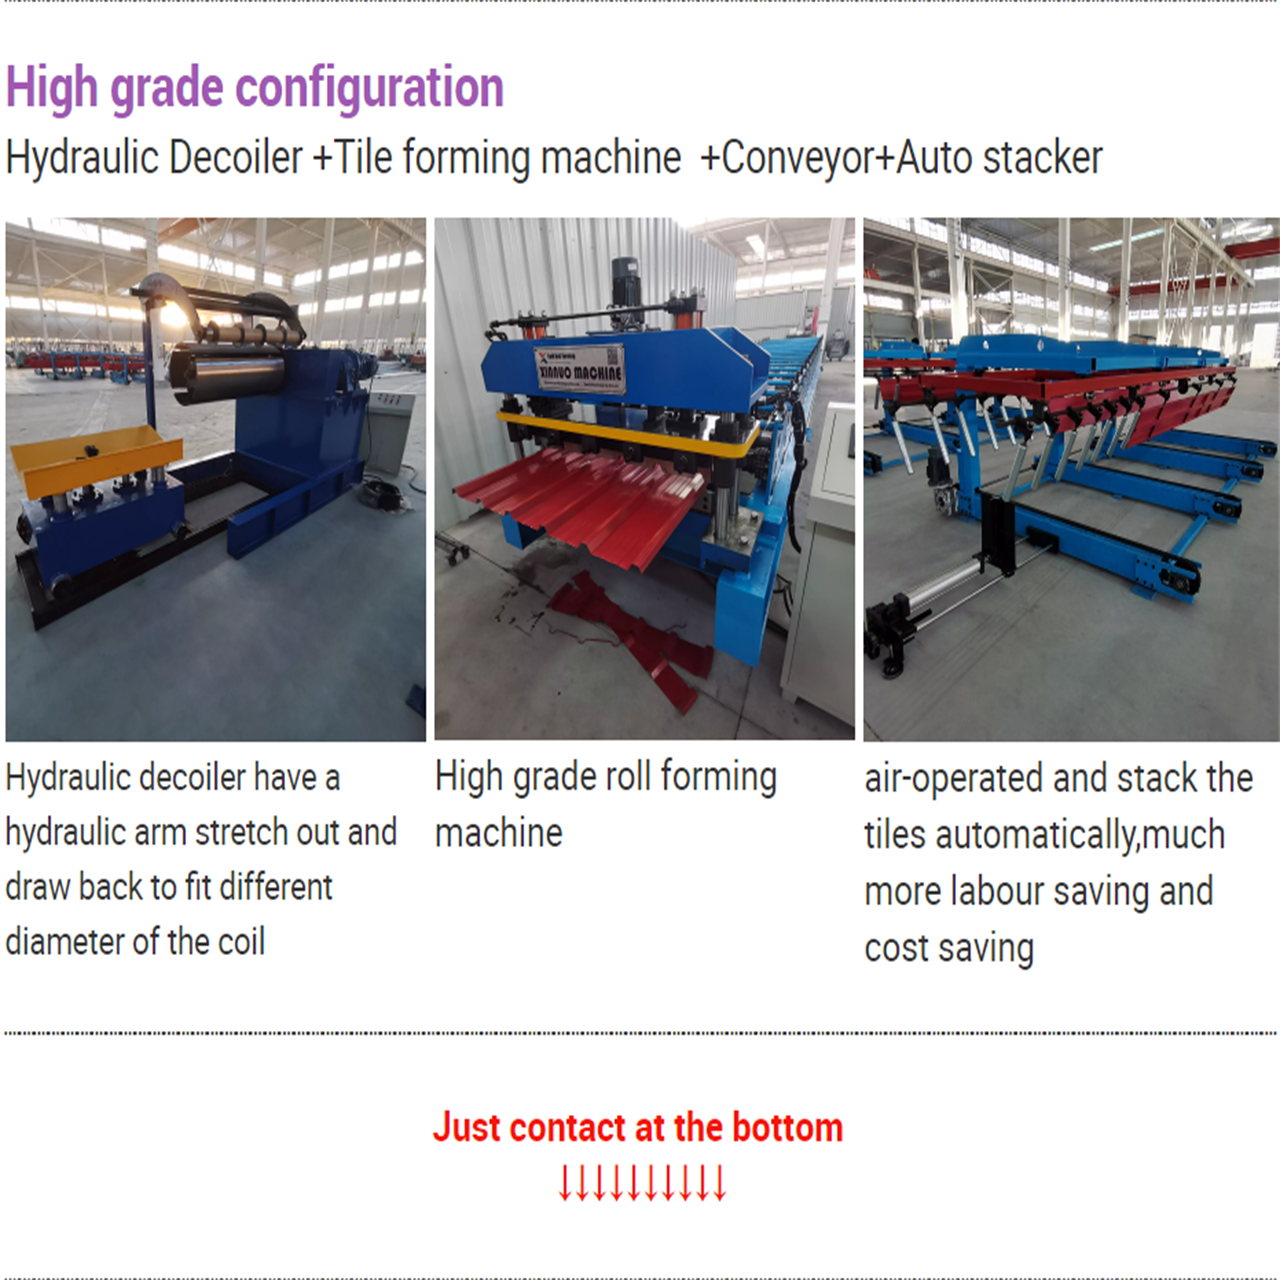
Decoiler machine — steel coil uncoiler for roll forming lines, built by the manufacturer and supplied factory direct to the Middle East. The decoiler is the first unit of a roll forming line. It carries the steel coil, holds it under control, and pays the strip off into the line at the rate the line consumes it. Every metre of finished profile made on the line passes through the decoiler first, which is why the decoiler is a production unit rather than a coil stand.
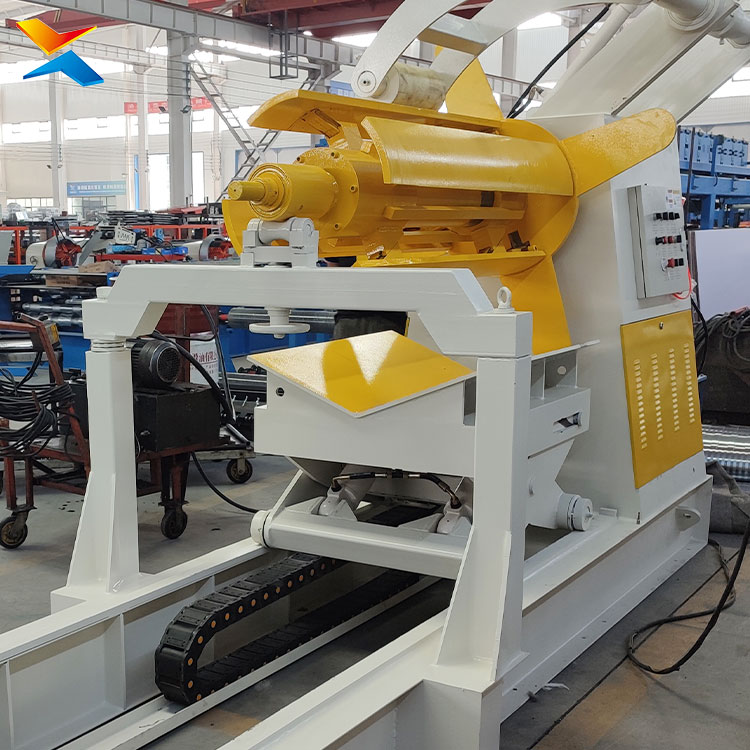
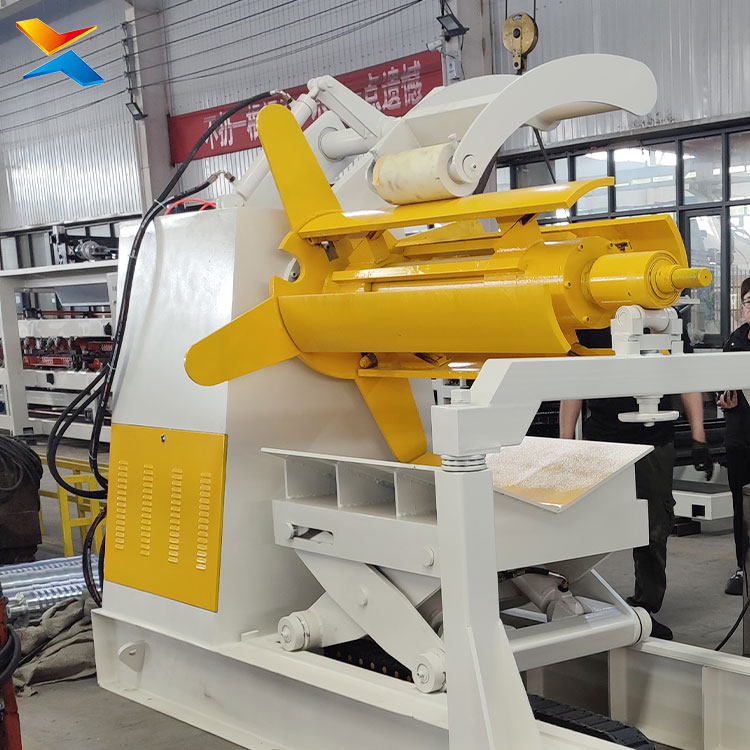
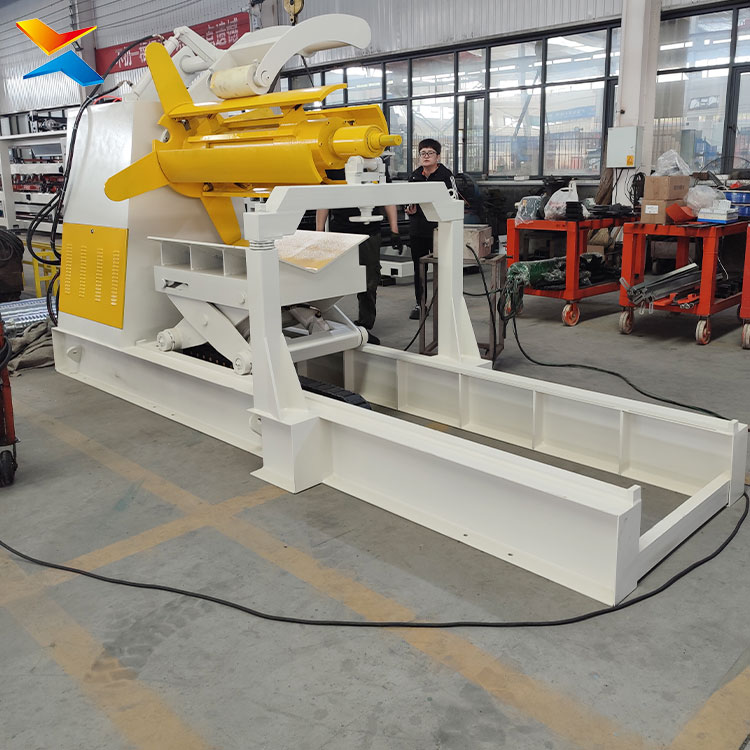
The machine consists of a frame and base, a spindle carrying an expanding mandrel, a loading arrangement for putting the coil onto the mandrel, and a braking and control arrangement that governs how the coil unwinds. The coil is placed onto the mandrel, the mandrel is expanded to grip the coil from the inside, the coil is lowered to working position, and the leading end of the strip is threaded into the line. From that point the line draws the strip, and the decoiler controls it.
What the decoiler does for the roll forming line.
A roll forming line cannot pull strip off a coil freely. If a coil is left to unwind on its own weight, the strip comes off loose, it can telescope sideways, the wraps can spring and tangle, and the strip arrives at the first forming station with slack in it that the forming stations cannot compensate for. A coil of steel strip has stored energy in it: it was wound under tension, and it wants to relax. The decoiler’s job is to let it relax in a controlled way.
So a decoiler does two things. It carries the coil so that the strand running into the line is delivered at the correct height and in the correct direction. And it applies a controlled resistance to the unwinding coil, so that the strip leaving the coil is held taut and the coil cannot overrun when the line slows or stops. This controlled resistance — the decoiler’s tension control — is the difference between a coil holder and a decoiler. A machine that only carries a coil will feed a coil of a certain weight and strip thickness; a decoiler with real tension control holds the strip steady across the line’s speed changes, through stop-and-start cutting cycles, and through changes in coil diameter as the coil gets smaller.
Why the decoiler’s position matters to the whole line.
The decoiler stands at the head of the line, and the strip enters every downstream unit from it. That has consequences that reach further than the decoiler itself.
Alignment. The decoiler must be set square and in line with the leveling unit and the forming machine, at the correct pass-line height. If the decoiler is positioned so that the strip leaves it angled or off-centre, the strip runs off-centre through the leveller, the forming stations and the shear, and the error is present in every piece the line produces. A decoiler that is mechanically sound but positioned badly produces a line that cannot make accurate profile. Line alignment is a decoiler installation concern, and it is settled with the layout drawing for the whole line.
Tension and the strip. The tension the decoiler applies influences how the strip behaves as it enters the line. Loose strip can fold or wander; over-tensioned strip is stretched and can be damaged or can distort the formed profile. The correct tension is the one that matches the strip and the line — and this is a setting that changes with strip thickness and with coil diameter, which is why tension control is a working function of the machine and not a one-time adjustment.
Coil change and line stoppage. Every coil change interrupts production, and the way the decoiler handles a coil change determines how long the interruption lasts. On a single-mandrel decoiler the line stops while the spent coil is removed and the new coil is loaded and threaded. On a double-mandrel decoiler the second coil can be prepared while the first is being consumed, so the change involves transferring the strip rather than loading a coil — a shorter stop. Which arrangement suits a workshop depends on how often the line changes coils, which follows from coil weight and from how much profile the line makes.
The coil parameters that define the machine.
A decoiler is specified by the coil it has to handle, and four parameters decide it. Each of them is a property of the coil the buyer actually receives, not of the finished product, which is why the buyer’s coil supply — not the profile — is the starting point.
The coil weight. This sets the structure of the machine: the frame and base, the spindle, the bearing arrangement and the mandrel. It also sets how the coil is loaded, because a coil beyond what can be handled safely by hand or by a simple hook must be loaded mechanically.
The coil’s inner diameter. This sets the mandrel, because the mandrel grips the coil from inside and expands to suit the inner diameter of the coil on it. A mandrel that does not reach the coil’s inner diameter cannot grip it; a mandrel larger than the coil’s inner diameter cannot be inserted. Inner diameter is a range, and coils from different suppliers in the same workshop can differ.
The coil’s outer diameter. This sets the working envelope of the machine: how far the coil projects from the mandrel, how much clearance the frame must provide, and how much the coil’s weight pulls against the spindle as it runs down.
The strip width. This sets how the coil sits along the mandrel and how the strip is guided as it leaves. It also has to match the line, because the strip that leaves the decoiler is the strip the whole line processes.
The coil parameters and the line are therefore specified together. A decoiler built for a coil range wider than the line needs will hold coil the line cannot use; a decoiler built for a range narrower than the buyer’s coil supply will refuse coil the workshop can buy.
Machine construction — the main assemblies.
The frame and base. A heavy welded steel structure carrying the spindle and the coil. The base is the reference for the machine’s position in the line, and it is built to distribute the coil load over the floor rather than concentrate it. The frame carries the bending load the cantilevered coil applies to the spindle.
The spindle and the expanding mandrel. The spindle is the shaft on which the coil is carried. The mandrel is the assembly mounted on it that grips the coil, and it expands radially to grip the coil from the inside and contracts to release it. The mandrel is the part of the decoiler that has to match the buyer’s coil, and it is the part on which the coil’s own weight bears while the coil turns.
Expansion mechanism. The mandrel is expanded and contracted by a mechanical arrangement, by a hydraulic arrangement, or by a pneumatic arrangement. A hydraulic mandrel expands with controlled force and grips the coil firmly, and its grip does not relax as the coil turns. The expansion mechanism is what holds the coil against the drag of tension control and against the inertia of a heavy coil starting and stopping.
The braking and tension arrangement. The resistance that holds the strip taut. It may be applied by a brake acting on the coil or the spindle, by a driven spindle operating in a controlled manner, or by a combination of the two, and it is adjustable so that the resistance can be set to the strip and to the line. This arrangement is the reason loose coils do not collapse into slack strip, and it is the part of the machine that most directly affects what the line receives.
The loading arrangement. The means by which the coil is put onto the mandrel. It may be a coil car that lifts the coil, carries it to the mandrel and positions it at the right height and centre, or a simpler arrangement in which the coil is brought up by the shop’s own lifting equipment. The loading arrangement also serves when the spent coil is removed, and it determines how much of a coil change is mechanical and how much depends on the operator.
Coil hold-down and stripping arrangements. Where a hold-down arm or a peeler is fitted, it keeps the outer wraps of the coil under control as the coil runs down and helps the strip to be fed and the last wraps to be released. These arrangements matter most on thin or easily creased strip and on coils reaching their end.
The hydraulic power unit. Where the mandrel expansion, the coil car or other functions are hydraulic, a pump station supplies them, arranged so that the hydraulic components are standard specification and can be sourced and serviced.
The control arrangement. The operator’s control of expansion, of the coil car, of the tension setting and of the line interlock. The decoiler is operated as part of the line, and its control arrangement is built to work with the line’s control so that the decoiler’s motions and the line’s start, stop and speed changes are coordinated.
Names for the same machine.
The machine is called a decoiler, a coil uncoiler, a coil reel, a payoff reel, a coil cradle or a coil stand, and in a roll forming context it is sometimes described simply by what it does — the coil feed at the head of the line. These names describe the same function, and they do not describe different classes of machine. The distinctions that matter to a buyer are not in the name but in three things: whether the mandrel expands and by what means, whether the machine has real tension control or only a carrying spindle, and how the coil is loaded onto it. Two suppliers can offer a “decoiler” that differ in all three.
Configurations.
Single mandrel. One mandrel carrying one coil at a time. The simplest arrangement and the one most roll forming lines use. The line stops for a coil change.
Double mandrel. Two mandrels on a rotating or traversing base, so a new coil can be loaded and prepared while the working coil is still being consumed. The strip is transferred from the spent coil to the new one, which shortens the interruption. Suited to lines that change coils frequently or that run continuously.
Mechanical, hydraulic or pneumatic mandrel expansion. The mandrel grips the coil from inside by one of these means. Hydraulic expansion gives a firm, controlled grip that stays firm while the coil turns.
Brake tension or driven tension. Tension is applied either by a brake resisting the pull of the line, or by driving the spindle in a controlled way, or by a combination. Driven tension control holds the strip steady across a wider range of coil weight and speed.
With or without a coil car. Whether the coil is loaded by a dedicated coil car or brought up by the shop’s own lifting equipment. This is decided by coil weight and by what the workshop already has.
With hold-down arm or peeler, and with strip guide arrangements. To keep the outer wraps under control as the coil runs down, help the strip feed into the line, and release the final wraps of the coil.
As part of a complete line. The decoiler is supplied as a unit of a roll forming line — with the leveling unit, the forming machine, the cutting arrangement, the run-out and the control system — or as a unit matched to an existing line.
Product features and advantages.
Built as a production unit of the line. The decoiler is made to run as the first unit of a roll forming line, with the pass-line height, the strip direction and the control arrangement set to work with the units downstream of it.
Controlled tension, not free unwinding. The machine applies a controlled resistance to the unwinding coil, so the strip arriving at the line is held taut, the coil does not overrun when the line slows or stops, and the strip is not delivered in slack folds.
Expanding mandrel that grips the coil from inside. The mandrel expands to grip the coil over its inner diameter, so the coil is held firmly and turns with the mandrel rather than slipping on it.
Hydraulic expansion with a grip that holds. Where hydraulic expansion is fitted, the grip is developed by oil pressure and is not relaxed by vibration or by the coil turning, which matters on heavy coils and on coils held against tension drag.
Coil parameters matched to what the workshop actually buys. The machine is built around the weight, inner diameter, outer diameter and strip width of the coil the buyer’s supply delivers, so the machine accepts the coil that arrives.
Coil car loading for heavier coils. Where a coil car is fitted, the coil is lifted, carried and positioned at the mandrel by the machine itself, so a coil change does not depend on the shop’s lifting equipment being free or on the operator handling a heavy coil.
Tension setting adjustable to the strip. The resistance can be set to suit the strip thickness and the line, which is what allows the same decoiler to run light and heavy strip without delivering loose strip on one and stretched strip on the other.
Heavy frame and spindle for the coil load. The frame and base are built for the coil weight and distribute it over the floor, and the spindle and bearing arrangement carry the weight of the coil as it turns.
Optional hold-down, peeler and strip guides. To keep the outer wraps controlled as the coil runs down and to help the strip feed and release cleanly.
Aligned to the line for straight strip travel. The machine is set square and in line with the leveling and forming units at the correct pass-line height, so the strip runs straight into the line rather than entering off-centre.
Built for the destination electrical supply. Machines are configured for the voltage, frequency and phase of the installation site.
Factory direct. The machine is built by the manufacturer and supplied direct, so the decoiler can be built to the buyer’s coil range and line rather than selected from a fixed catalogue, and technical questions are answered by the people who build it.
The decoiler in Middle East conditions.
The machine is supplied into Middle East roll forming shops, and the conditions it works in there affect both how it is configured and how it is kept working.
Coastal humidity and salt air. Much of the region’s roll forming is carried out near the coast, where the air carries salt. Coil arrives with its coating, but the decoiler is exposed steel: the frame and base where the protective finish is thin, the exposed surfaces of the spindle and mandrel, unpainted metal on the coil car and the guides, and the electrical enclosures. Protective finish and routine attention to exposed surfaces are therefore specification and maintenance matters in this market.
Inland heat. Inland, workshops run at high ambient temperatures for long periods, and hydraulic expansion and any hydraulic drive in the machine add their own heat. High oil temperature thins the oil and reduces the firmness of a hydraulic grip and the consistency of driven tension. Machines built for this market are configured with attention to the hydraulic arrangement and to how the machine sheds heat.
Wind-blown dust and sand. Dust and sand work gradually into the mandrel expansion mechanism, into the spindle bearing arrangement, into the coil car guides and into the control panel. The effect is progressive: expansion and contraction become less free, the mandrel grips less evenly, and the guides become harder to move. Machines for the region are built with attention to how these mechanisms are protected.
Wide day-to-night temperature variation. Considerable swings between a hot working day and a cool night work the fastenings and fits of a heavy machine, and on a decoiler this is felt in the mandrel expansion, in the spindle arrangement and in the coil car.
Coil storage and handling. The region’s heat and dust also affect the coil before the decoiler ever sees it. Coil stored in a hot, dusty yard or an open shed arrives with dust on the wraps and with its coating aged by sun and heat, and a decoiler cannot correct the condition of the coil it is given. Keeping coil under cover and handling it without damage is part of getting good strip into the line, and the decoiler is where a damaged coil becomes damaged profile.
Where the machine is used across the region. Middle East roll forming production is concentrated where the region’s construction and industry are: roof and wall panel lines for industrial buildings, warehouses and commercial construction, purlin and structural section lines for steel building work, floor deck lines, composite and insulated panel lines, and lines producing profiles for the region’s industrial and infrastructure projects. Every one of those lines begins with a decoiler, and no profile leaves the line until the strip has passed through it.
Machine build quality.
The decoiler is built as a heavy fabricated machine rather than assembled from light components. The frame and base are welded from steel plate and sections, built to carry the coil load without deflection and to hold the spindle in alignment. The locating and mounting surfaces are machined, and the spindle and the mandrel assembly are made as a matched arrangement so that the mandrel grips evenly around the coil and runs true. The expansion mechanism and the braking arrangement are built for the coil range the machine is made for. The hydraulic system is assembled from standard-specification components. The electrical arrangement is wired and tested as a complete unit, and the machine is run and checked before shipment so that mandrel expansion, tension setting, the coil car motion where fitted, and the control and interlock arrangement are verified as a complete machine.
Service and support.
Machines are supplied with documentation covering the machine, including the operating manual, the electrical drawings and the hydraulic arrangement. Installation and commissioning are carried out with technicians attending site, and operator training is provided so that the coil is loaded safely, the mandrel is expanded correctly, and the tension setting is made for the strip and the line. Illustrated manuals and video guidance cover the settings used most often, including the tension setting and its relation to strip thickness and coil diameter, and the routine attention the machine needs in a hot and dusty workshop. Engineering support is available for technical questions through the working life of the machine, and spare parts are supplied, with the mandrel components, the expansion mechanism and the hydraulic components given particular attention.
♦ COMPANY PROFILE:
Hebei Xinnuo Roll Forming Machine Co., Ltd., not only produce different types of professional roll forming machines, but also develop intelligent automatic roll forming production lines, C&Z shape purline machines, highway guardrail roll forming machine lines, sandwich panel production lines, decking forming machines, light keel machines, shutter slat door forming machines, downpipe machines, gutter machines, etc.
Advantages of Roll Forming A Metal Part
There are several advantages of using roll forming for your projects:
- The roll forming process allows operations such as punching, notching, and welding to be performed in-line. Labor cost and time for secondary operations are reduced or eliminated, reducing part costs.
- Roll form tooling allows for a high degree of flexibility. A single set of roll form tools will make almost any length of the same cross-section. Multiple sets of tools for varying length parts are not required.
- It can provide better dimensional control than other competing metal forming processes.
- Repeatability is inherent in the process, allowing easier assembly of roll formed parts into your finished product, and minimizing problems due to “standard” tolerance build up.
- Roll forming is typically a higher speed process.
- Roll forming offers customers a superior surface finish. This makes roll forming an excellent option for decorative stainless steel parts or for parts requiring a finish such as anodizing or powder coating. Also, texture or pattern can be rolled into the surface during forming.
- Roll forming utilizes material more efficiently than other competing processes.
- Roll formed shapes can be developed with thinner walls than competing processes
Roll forming is a continuous process which converts sheet metal into an engineered shape using consecutive sets of mated rolls, each of which makes only incremental changes in the form. The sum of these small changes in form is a complex profile.