Glazed Tile Roll Forming Machine for Sale | Glazed Roof Tile Making Machine Supplier UAE Saudi Arabia
Product Description
Glazed roof tile making machine for sale, factory-direct from the manufacturer, supplied to steel building projects in the UAE and Saudi Arabia.
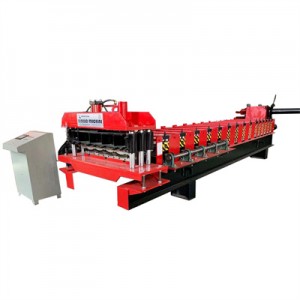
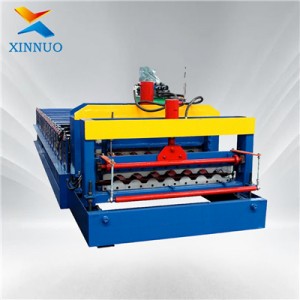
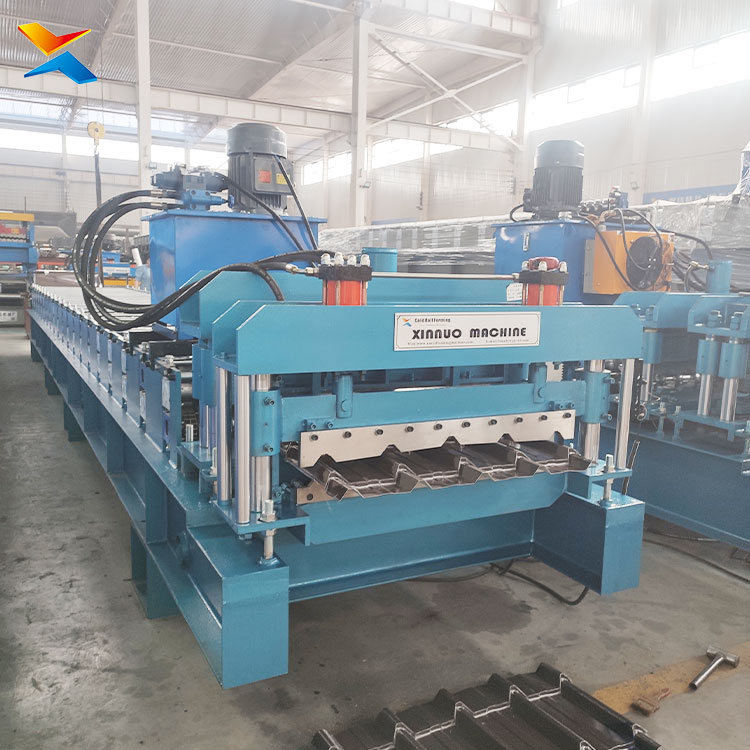
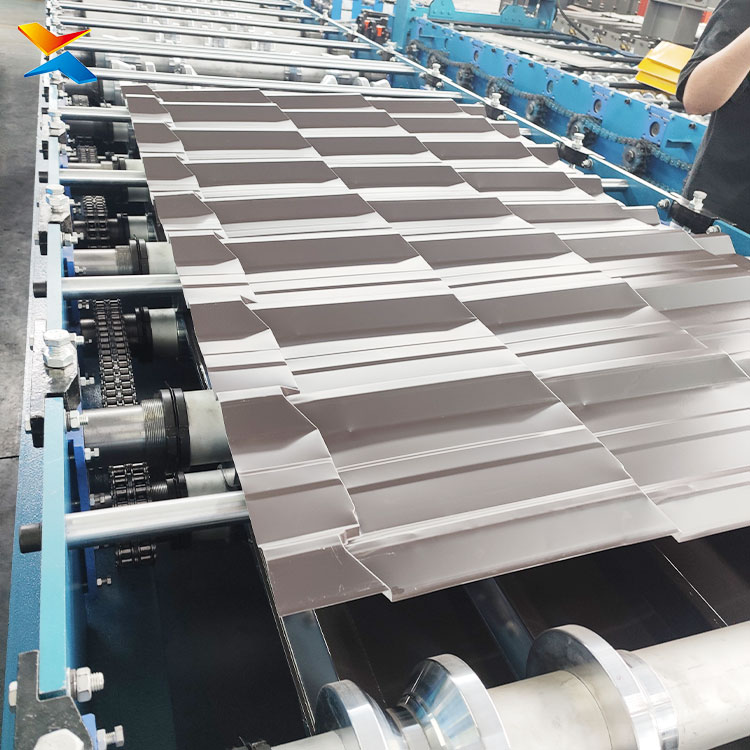
This glazed tile roll forming machine forms coated steel coil into roof and façade panels that carry the look of traditional glazed roof tile. It runs in two rhythms: continuous rolling forms the curve, and a pitch-stamping device presses a segment line into every peak, so each panel reads as a row of individual antique tiles rather than a plain wave. The device is what makes it a glazed tile machine, and it is also what places this machine above a comparable arc machine in price.
The panel it produces is metal. It is lightweight colour-coated steel coil — not fired clay, not ceramic, and not PVC or resin. That is the reason a Gulf steel building uses it at all: the appearance of traditional roof tile without the weight and fixing penalty of real tile, so a villa roof, a mosque roof, a hotel elevation or a whole façade can carry a traditional idiom on a light steel structure. For buyers who must serve two material markets from one machine, the range also includes a build that is recorded as switchable between colour-coated steel glazed tile and resin tile by adjusting the pitch.
Buy the right category first — this is where most of the money is lost.
Before comparing quotations, settle which of the curved products you actually need, because they are different machines at different price levels. A continuous curved wave with no tile pattern is made on an arc roll forming machine. A curved tile with antique texture — with the segment lines on every peak — is made on a glazed tile machine, which carries the extra pitch-stamping device. A curved tile with stronger relief also belongs to the glazed tile family: an asymmetric arc, where one flank is steeper than the other so the relief reads deeper, and a bamboo-joint profile, which carries the deepest relief in the range on a wide pitch.
The naming convention makes this readable at a glance in any quotation you receive. If the machine name contains “峰” (peak), it is a glazed tile machine. If it contains only “波” (wave), it is an arc machine. A glazed tile machine sits above a comparable arc machine in price, and a servo-driven version sits above the standard version — so this single distinction is the largest commercial decision in the purchase, and it should be settled before the specification is discussed.
Peak height decides how the machine is built.
The deeper the peak, the more forming rows the machine needs in order to produce a flat, consistent panel without marking or distortion. Row count in turn drives the frame class, the shaft diameter and the motor power, so those four items should always be compared as a set rather than separately. Economy builds run on channel-steel or light frame sections. Standard builds step up to heavier frames. Medium-heavy and deep-arc work moves to heavy frames, and the heaviest builds in the range use a portal-style heavy frame that the factory’s records describe as an industry-heavy specification rather than a common one.
A useful check when a quotation arrives is to line up forming rows, frame class, shaft diameter and motor power against the peak height your section requires. Where a quotation offers a light row count for a deep peak, it is a different class of machine, whatever the headline price suggests. On deep-arc work, mass belongs to the same argument: these machines are built heavy, and that mass is what keeps the forming stations from deflecting under a deep peak.
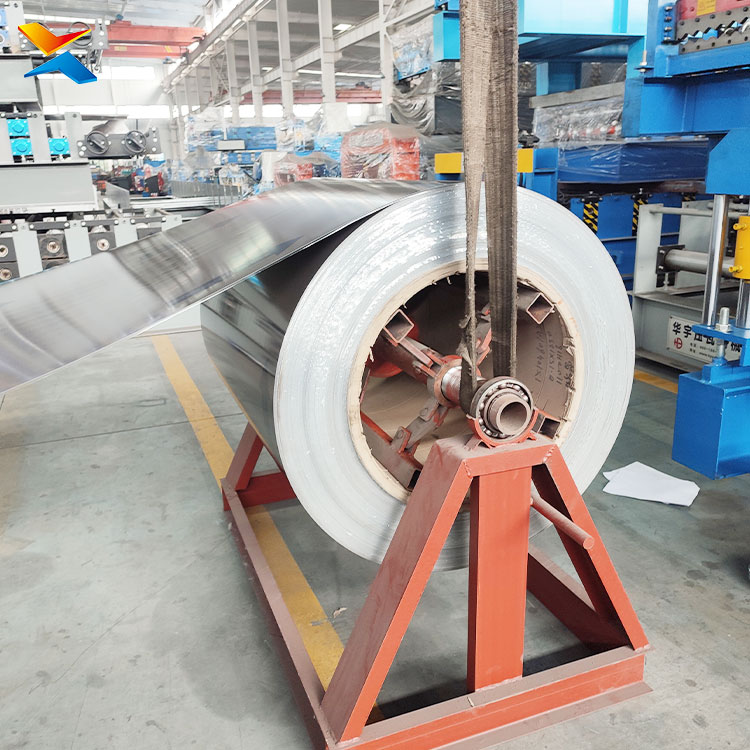
The material this family forms is thin-gauge colour-coated steel coil. A deep peak deforms material heavily and is not suited to thick plate, while the heaviest builds extend to a somewhat thicker gauge because their frames and drives are built to move that material. Confirm the gauge you will actually run for the specific model in writing, rather than inferring it from a general figure.
Pitch is a designed mould, not a variable you can name freely.
Pitch decides how the finished tile looks. Small pitches give a fine, dense antique appearance suited to high-end façades and roofs in a Tang or Song idiom. Medium pitches are the mainstream specification — the volume seller of the range and the balance most buyers choose. Large pitches give broad, high-relief peaks in a Qing-style idiom for temples, villas and garden buildings.
Each pitch corresponds to a designed stamping mould, and the factory’s own record here covers long-standing pitch design experience across a wide span of values. A pitch that is not already in the archive means new tooling — a separate engineering step that should be answered in writing rather than assumed into a delivery date.
Because the pattern is what customers see, the drive decides the result on a large roof. A servo motor with bevel-gear drive positions the pitch far more precisely than a clutch-and-brake arrangement, and the difference becomes visible over the many repetitions required across one elevation. The bevel gear train is also documented as quieter and smoother in service than chain drive. Buyers who need throughput rather than maximum pattern precision can choose the newer higher-power builds in the range, which run faster and handle slightly thicker material, and the most recent addition uses an SEW-compatible helical gear reducer for better efficiency and a quieter, longer-lived drive.
Curved variants available for Gulf projects.
The range holds several curved variants that answer specific briefs. An asymmetric arc, with one flank steeper than the other, gives a stronger sense of depth and is recorded for high-end commercial and residential work. A bamboo-joint profile carries the deepest relief in the range on a wide pitch, for gardens, temples and boutique hospitality. A “with A” version presses an A-shaped reinforcing rib across the flat between peaks, raising panel stiffness without increasing peak height. A half-peak design fits a partial peak at each edge so adjoining panels join into complete peaks and coverage improves. A dual-width build produces two panel widths from one machine by changing part of the tooling, which avoids buying a second machine where a project specifies more than one width. And the resin-and-glazed dual-purpose build serves buyers who supply both material markets.
Where the panel is used on steel buildings in the Gulf.
The mainstream use is the project that specifies a traditional idiom: villa roofs and elevations, mosques and religious buildings, tourist and heritage developments, boutique hospitality, and new-Chinese-style façades. In these projects the panel is formed to the building’s own lengths, closes the roof or elevation quickly, and takes its colour from the coil coating system rather than from tiles laid piece by piece.
There is a second use that matters in this region. A small arc with a dense wave suits integrated housing and light-steel roofs, where this family competes directly with single-layer trapezoidal panels — the advantage being the more attractive arc, at a comparable weight. The factory’s records note this dense-wave work as common in the Middle East market, which is why the range includes it as a standard offering for Gulf buyers rather than an exotic option.
What being a supplier for the UAE and Saudi Arabia means in practice.
It means the machine is configured for your project and your site, not sold from a fixed catalogue. The panel is formed to the lengths your building needs. Sections are matched against an existing production-proven blueprint where possible, and where they are not, the gap is stated in writing before an order is placed. Electrical configuration is set to your workshop supply. Documentation, certification and reference projects are provided on request rather than assumed. Installation, commissioning and operator training are part of the company’s service model, with around-the-clock engineering support and spare parts supply after handover, and the specific scope should be written into the order rather than left to assumption.
Two exposure conditions shape the specification in this region. Near-coast humidity and salt-laden air on UAE projects, and intense solar loading with strong thermal cycling inland in Saudi Arabia, both put the emphasis on the coil and coating system the buyer chooses. The machine forms the geometry; the coating decides how long the appearance lasts. A lifespan question answered with a number rather than with a coil specification is an answer to a different question, and this page deliberately does not quote service life, because it is not a property of the machine.
Products from this family have been supplied to Dubai and to the wider region, alongside other export markets with traditional-architecture demand. Those are archive records of what was built and for which market, not a claim about installed base or market share.
The process behind the profile.
The manufacturing standard is the same one used for the factory’s single-layer panel machines. Forming dies are forged from carbon steel and carried through a multi-step process of rough turning, hardening, finish turning, keyway cutting, polishing and electroplating. Shafts are alloy steel, finish-turned and externally ground for roundness and straightness under load. Frames are machined on CNC gantry mills so that every forming station measures from a flat reference. Welding is shielded and slag-free, and surfaces are shot blasted, then electrostatically sprayed and baked for protection.
To quote a machine, send these items. The appearance type you want — antique tile texture or a plain curve — because that decides the category. A cross-section drawing or sample, or the closest available reference: peak count, pitch, peak height and effective width. The material and the gauge you will actually run. The coil width obtainable in your local market, since the machine’s feed width must match a coil you can actually buy. Your drive preference — standard chain, or servo with gear. The panel lengths required and your daily output. Your workshop’s voltage and frequency. And any dual-purpose requirement, whether two widths, two wave scales, or metal and resin tile. The engineers will identify the closest production-proven blueprint, confirm in writing whether your section matches the archive or needs new pitch tooling, and return an itemised factory-direct quotation with the line layout drawing for your configuration.
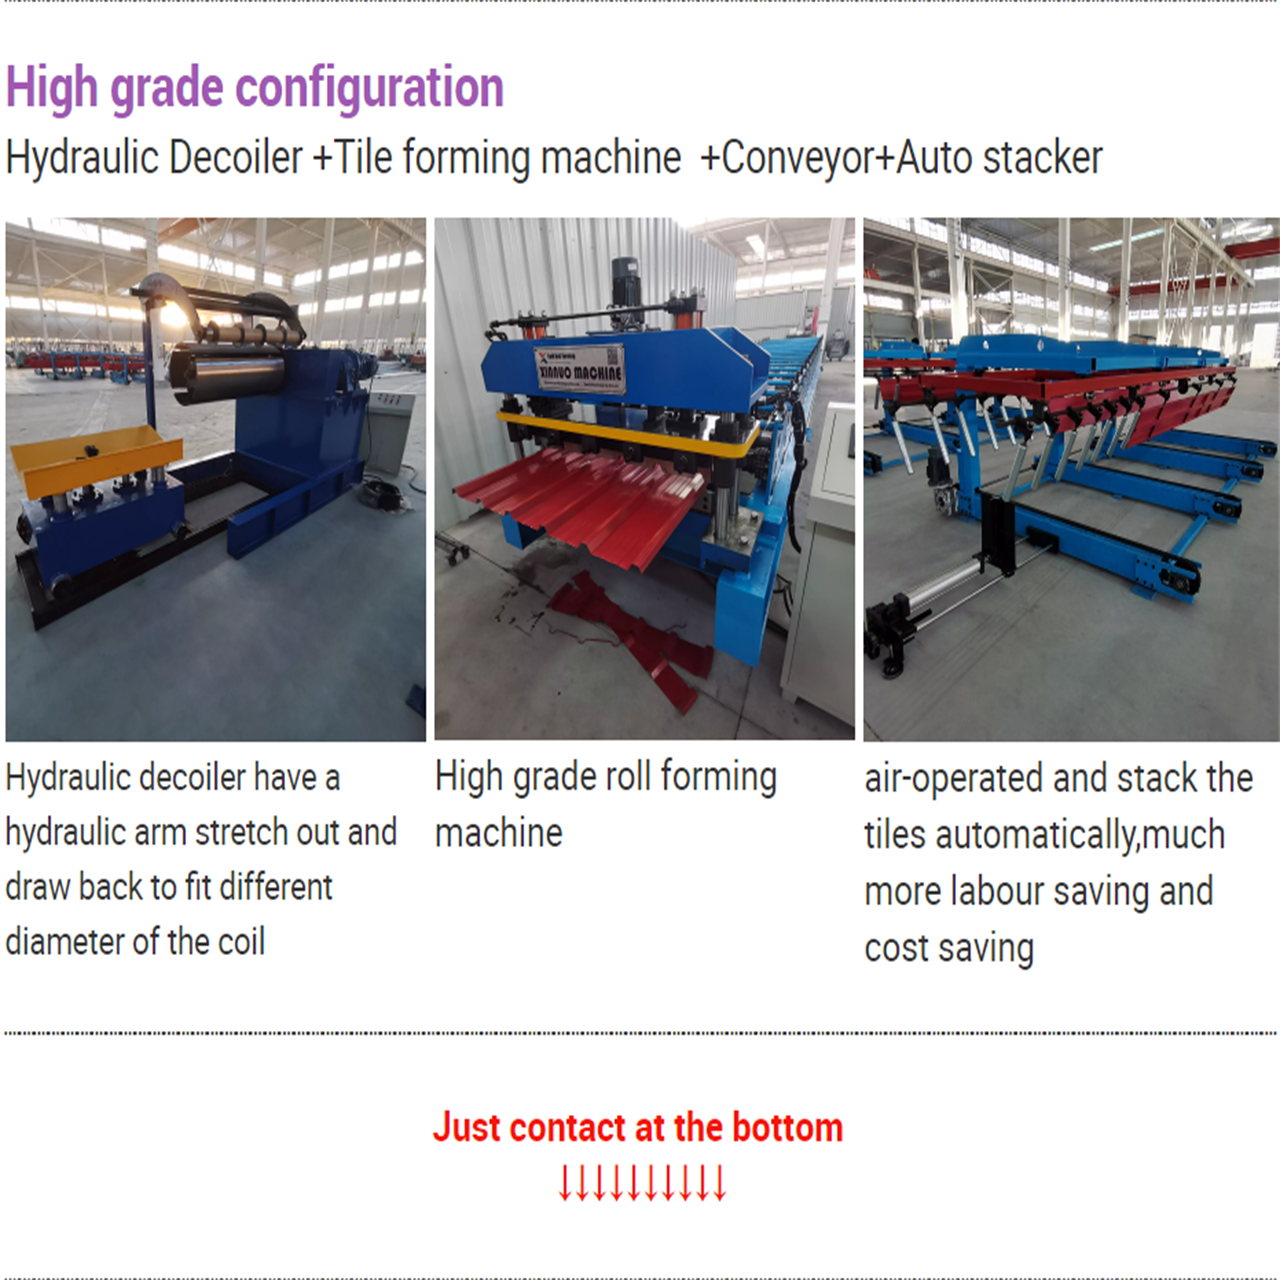
♦ COMPANY PROFILE:
Hebei Xinnuo Roll Forming Machine Co., Ltd., not only produce different types of professional roll forming machines, but also develop intelligent automatic roll forming production lines, C&Z shape purline machines, highway guardrail roll forming machine lines, sandwich panel production lines, decking forming machines, light keel machines, shutter slat door forming machines, downpipe machines, gutter machines, etc.
Advantages of Roll Forming A Metal Part
There are several advantages of using roll forming for your projects:
- The roll forming process allows operations such as punching, notching, and welding to be performed in-line. Labor cost and time for secondary operations are reduced or eliminated, reducing part costs.
- Roll form tooling allows for a high degree of flexibility. A single set of roll form tools will make almost any length of the same cross-section. Multiple sets of tools for varying length parts are not required.
- It can provide better dimensional control than other competing metal forming processes.
- Repeatability is inherent in the process, allowing easier assembly of roll formed parts into your finished product, and minimizing problems due to “standard” tolerance build up.
- Roll forming is typically a higher speed process.
- Roll forming offers customers a superior surface finish. This makes roll forming an excellent option for decorative stainless steel parts or for parts requiring a finish such as anodizing or powder coating. Also, texture or pattern can be rolled into the surface during forming.
- Roll forming utilizes material more efficiently than other competing processes.
- Roll formed shapes can be developed with thinner walls than competing processes
Roll forming is a continuous process which converts sheet metal into an engineered shape using consecutive sets of mated rolls, each of which makes only incremental changes in the form. The sum of these small changes in form is a complex profile.