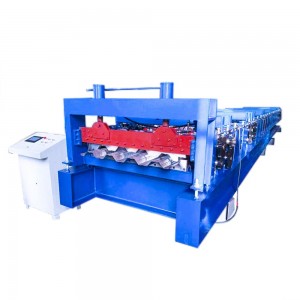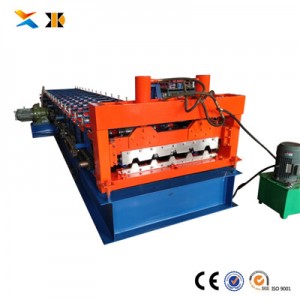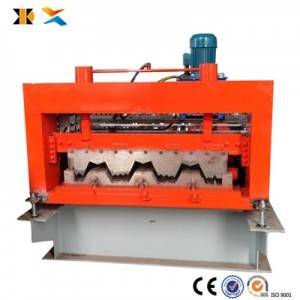
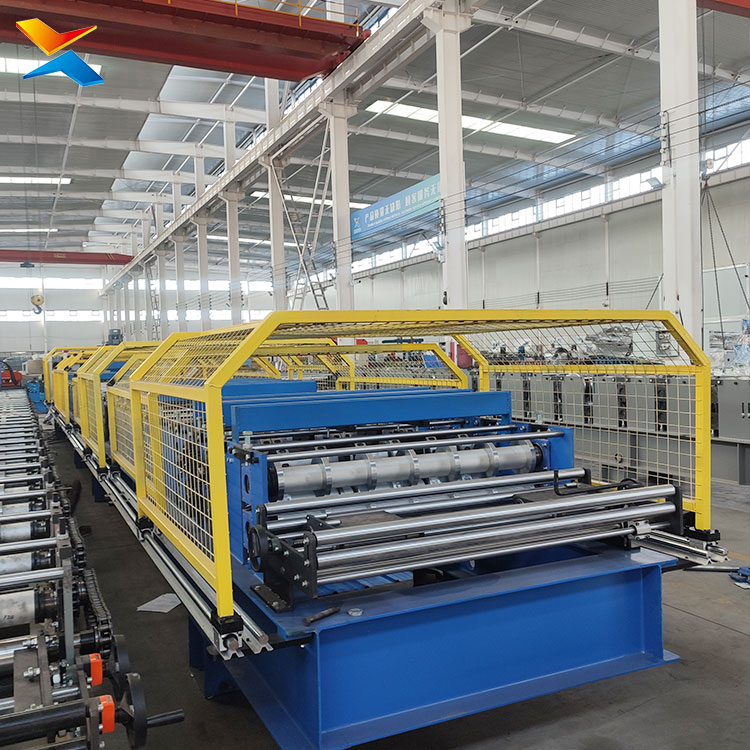
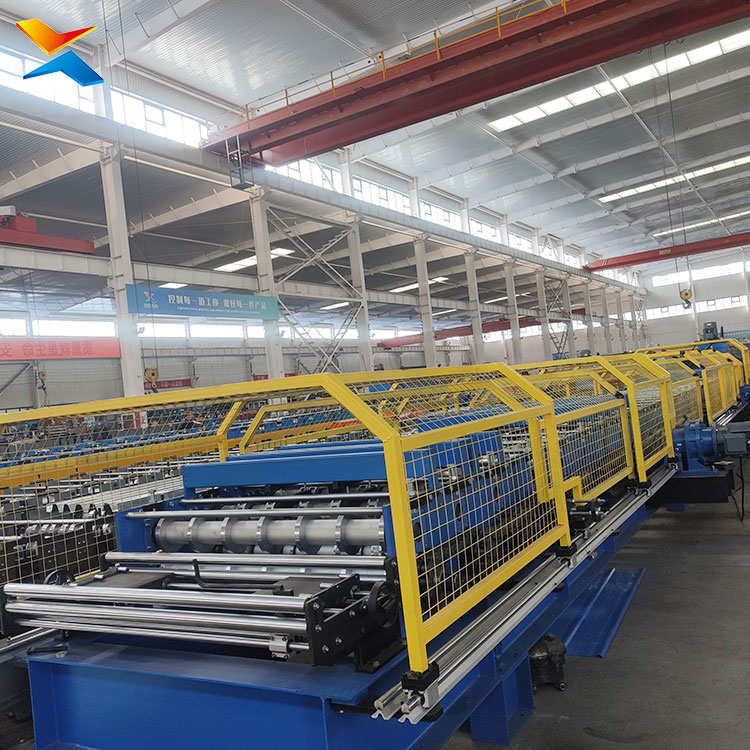
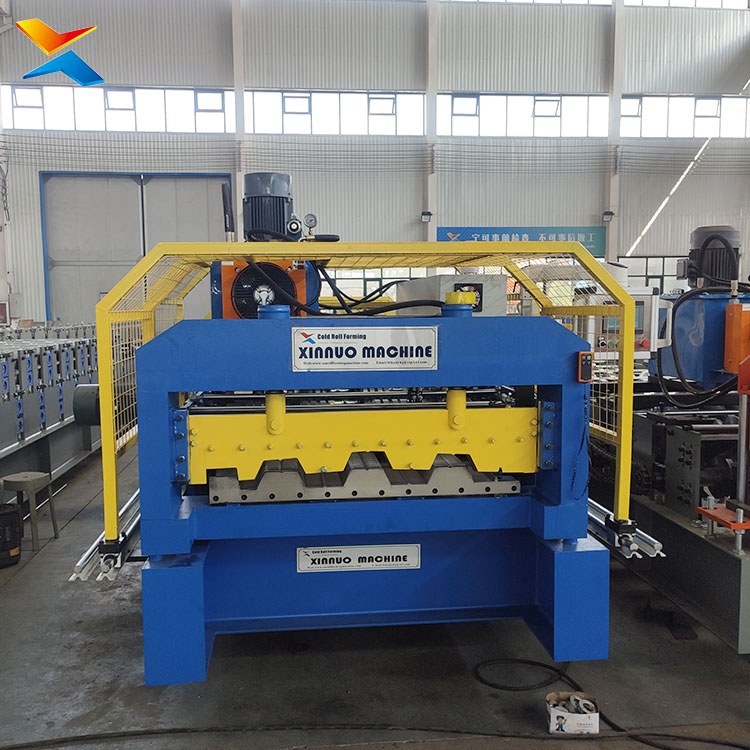
Floor decking roll forming machine for steel structure building floors, built by the manufacturer and supplied factory direct to the Middle East.
The machine forms galvanized steel strip into floor deck panels — the profiled steel sheets that a steel-frame building lays across its beams and pours its concrete floor onto.
A floor deck is not a roof sheet, and it is not a floor finish. It does two structural jobs.
Before the concrete cures, it is the formwork. The deck spans between the beams and carries the wet concrete, the placing equipment and the construction crew. At that stage it is a structural member in its own right, and the deflections it develops are the deflections the wet slab takes.
After the concrete cures, it becomes tensile reinforcement. The steel and the concrete act together as a composite slab: the concrete takes the compression, the deck takes the tension. For that to happen the two materials must not slip against each other, which is why the deck’s ribs carry pressed embossments — the dimples that grip the concrete and force it to move with the steel.
That second job is the one that is easy to miss, and it is the one the machine’s tooling is really for. A panel with a convincing profile but shallow or inconsistent embossments is a panel that will carry the wet concrete and then fail to bond with it. On site, that reads as a slab that is weaker than the design assumed, and nothing about the panel’s appearance shows it.
The two profile families.
Open deck. Trapezoidal ribs with open troughs between them. It is the simpler profile to form, the more common one worldwide, and the one that costs less per square metre of floor.
Closed deck. A re-entrant, dovetail-shaped rib whose mouth closes over, so the concrete wraps around the rib end and locks onto it. The interlock gives a higher composite ratio and a stiffer slab for the same depth of construction, which is why closed deck is used for long-span floors, elevated parking structures and high-rise composite floors where the shear stud count has to be kept down.
Closed deck is where the machine’s capability is tested. The re-entrant shape cannot be formed by a simple sequence of bending passes: the rib has to close over itself, which needs more forming rows, heavier shafts and a locking roller set built for that geometry. A machine that forms open deck well is not automatically a machine that can form closed deck.
Why a floor deck machine is a heavier class of machine than a roof panel machine.
The two look similar from across a workshop floor, and they are not the same machine. Three differences drive everything else.
The ribs are much deeper. A roofing profile’s rise is measured in a small number of millimetres; a floor deck’s rib is several times deeper, because the rib has to develop the slab’s structural depth. Forming a deep rib means moving a great deal of material a long way, which cannot be done in a few passes.
The material is much thicker. Floor deck is formed from substantially heavier gauge than roofing, because it has to carry wet concrete and then act as reinforcement. Thick material at high forming loads is what forces the heavier frame, the larger shafts and the heavy chain.
The friction is much greater. A deep rib formed in thick strip generates far more friction between the strip and the rolls than a shallow roofing profile ever does. That friction is the source of the floor deck machine’s defining problem.
Pooling — the problem that defines this machine.
In floor deck production the strip can stop advancing while the rolls continue to turn: the material jams in the machine, and the run is lost until it is cut out. The cause is built into the product. A deep profile in thick material needs high driving force, and any row that is pushing the strip faster or slower than its neighbours becomes a brake on the whole line.
The anti-pooling design addresses this with several interlocking measures rather than one.
A clutch after the embossment wheel row. The embossment wheel is larger in diameter than the forming wheels around it, so if it were driven directly from the same chain it would try to rotate faster than the strip is moving and would jam the material against the next row. The clutch disengages it once the material has passed, so the embossment wheels are carried by the downstream rolls at the strip’s own speed instead of driving it.
Bearing-mounted oversized wheels in the rear forming rows. These wheels carry internal bearings and are sized larger than the rows ahead of them, which changes their function from pulling the strip to pushing it. Pushing at the rear supports the strip without dragging its surface, and it removes the scratch marks that a pulling arrangement leaves on galvanized steel.
Pressure reinforcement bars. Bars fitted at the embossment row, the main drive, the rib-forming rows and the sizing rows raise the shafts’ effective leverage, so a shaft of a given size behaves like a larger one and the panel’s flat areas stay flat instead of bowing between ribs.
Gear drives at the load-critical rows. Gear transmission at the embossment row, ahead of the oversized wheel section and at the exit rows raises the feeding and pulling force where thick, deep-profile strip demands it.
A dual-cylinder floor-standing shear. Two hydraulic cylinders share the cutting force so the cut is balanced across the panel’s width, and the shear sits at floor level so the finished panel drops and stacks by gravity rather than being lifted off.
The embossments, and why their wheel is the critical part.
The embossments are pressed into the rib walls and the flat areas to grip the concrete. Their depth, their spacing and their consistency along the panel are what convert the deck from formwork into reinforcement.
The wheel that presses them is the machine’s most sensitive component, for a geometric reason: it has to be larger than the forming wheels beside it in order to press into the rib, and a larger wheel driven from the same chain turns faster at its surface than the smaller wheels do. Left driven, it fights the strip. The clutch is the answer, and it is the difference between a machine that runs and a machine that jams.
The profile number is a width, not a grade.
Floor deck profiles are named by their effective coverage width — the width one panel actually covers once it is lapped onto the next. The number says nothing about the rib depth, the material thickness or the structural capacity. Two profiles with the same nominal width can differ in rib height and in open or closed form, and therefore in what they can span.
The material is galvanized, not colour-coated.
Floor deck is never seen: it is poured over and then becomes part of the slab. Its coating is therefore a corrosion protection for the construction period and for the life of the slab, not a finish. Galvanized strip is the material, and the zinc coating is what has to survive the forming without being cut through at the rib corners, because a break in the coating at a bend is where rust starts inside a floor that nobody will inspect.
Forming quality that shows up on site rather than in the workshop.
Rib straightness along the length. A rib that wanders is a rib that will not sit on the beam line it was set out for, and a deck that will not sit down flat over its supports leaves a gap that has to be packed. Straightness comes from the frame holding the stands in line, not from the tooling alone.
Consistent embossment depth. Embossments that vary along a panel give a slab whose composite action varies with them, and the variation is invisible after the pour. The clutch and the pressure bars exist to hold that consistency through a long run.
Camber and flatness of the pan. The flat areas between ribs are what the concrete sits on and what the deck’s width is measured across. A pan that bows between the ribs takes up concrete that the design did not allow for.
Square and clean ends. The panels butt end to end along the beam, and an end that is not square opens a gap that has to be closed with a end stop before the pour.
Consistent effective width. Because panels lap, an effective width that drifts means the laps tighten or open along the floor, and the coverage the design assumed no longer holds.
The shear and the panel’s handling.
The dual-cylinder floor-standing shear cuts the panel square across its full width with the force shared between two cylinders, and because it sits at floor level the cut panel falls to the stacking position under its own weight. On a panel of this weight, that is not a convenience: lifting a deep-ribbed deck panel off a shear by hand distorts the ribs that the slab depends on.
Machine construction.
The frame is a heavy H-section structure machined so the stands sit in line and hold their centres, sized for the forming load a deep rib imposes rather than for a roofing profile. The mid-plate that carries the drive is thick, because it takes the torque of two motors rather than one. The shafts are large-diameter alloy steel, rough turned, precision ground and plated, because a shaft that flexes under a deep-rib load lets the rolls open and the rib lose its depth. The forming wheels are forged from carbon steel and carried through the full sequence — rough turning, hardening, finish turning, keyway cutting, polishing and plating — so the working surface holds its shape in service. The embossment wheels are made as a matched set with the forming wheels around them, because their diameter relative to their neighbours is what the clutch timing depends on.
Configurations.
Standard single-layer machine. One profile, one set of tooling, one deck type. The arrangement for a producer supplying one deck specification to a project or a market.
Closed-deck build. Additional forming rows, heavier shafts and the locking roller set that the re-entrant geometry requires.
Heavy-profile build. A heavier drive and frame for the deepest ribs and the thickest strip in the range, where the standard arrangement would be the limit.
Double-layer machine. Two profiles stacked in one frame for a producer who needs both, one at a time. It is a different machine from this one, and it is chosen when the product range — not the floor — calls for two decks.
Product features and advantages.
Two structural jobs in one panel. The profile carries wet concrete as formwork and then acts as tensile reinforcement, with the embossments providing the bond that makes the composite slab work.
Open and closed profiles from the same family. The trapezoidal open deck and the re-entrant closed deck are both covered, and the closed deck is built with the extra rows and the locking roller set its geometry needs.
Anti-pooling design as a system. The clutch, the bearing-mounted rear wheels, the pressure bars, the gear drives and the dual-cylinder shear work together against the jamming that deep ribs in thick strip produce.
An embossment wheel that does not fight the strip. The clutch takes the oversized wheel out of the drive once the material has passed, so it is carried at the strip’s speed instead of dragging against it.
Dual-motor drive on a heavy frame. Two motors share the forming load, on a frame and mid-plate sized to take their torque.
A floor-level shear that stacks by gravity. The panel drops to the stack without being lifted, so the ribs are not distorted in handling.
Galvanized strip formed without cutting the coating. The roll sequence and the pressure bars are set to form thick galvanized material without breaking the zinc at the rib corners.
The machine in Middle East conditions.
The floor deck is a construction-stage product, and that is what the region’s conditions act on. Unlike a roof, the deck spends its working life hidden inside a slab. Its exposure is concentrated in the weeks between laying and pouring: it sits on the frame in direct sun, it is walked on, it collects dust and it takes the heat of the day and the cool of the night across its span.
Heat before the pour. A galvanized deck in direct sun runs well above air temperature and expands across the span it is laid over. A deck laid tight in the cool of the morning and then heated can buckle at the ends if the layout leaves it no room to move, and the buckle is in the panel that is about to be concreted. The layout and the end stops are what accommodate it.
Dust and sand before the pour. Dust that settles into the troughs is dust that ends up at the bottom of the slab, between the steel and the concrete, exactly where the bond is supposed to develop. The deck’s cleaning before the pour is a construction matter, but a profile with deep open troughs holds more of it than a closed profile does.
Coastal air and stored coil. The galvanized coil is the material, and it is stored before it is formed. In coastal areas the coil’s edges and its exposed wraps are where white rust and then red rust begin, and a coil stored poorly forms a panel whose corrosion started before it was made. Coil storage is part of what the finished floor’s durability rests on.
Long spans and the region’s floor plates. Steel-frame floors in the region’s commercial and residential buildings often run over spans where the slab’s stiffness, not its strength, governs. That is the condition in which the closed profile earns its cost, because the interlock raises the composite ratio and the slab depth can come down.
Where the panel is used.
Steel-frame multi-storey buildings; mezzanine floors inside warehouses and industrial buildings; elevated car parks; high-rise composite floors; plant floors and equipment platforms; modular and prefabricated buildings; and floor plates where the deck has to span between beams without propping.
Service and support.
The machine is supplied with installation and commissioning support, operator training, illustrated manuals and a spare parts list, and with engineering support for the profile a project requires. Because the embossment wheel and the forming wheels around it are made as a matched set and the clutch timing depends on their relative diameters, the tooling record is part of what is handed over: it is what allows the same deck to be produced again for a later phase, and it is what keeps the clutch set correctly when wheels are replaced.
Factory direct.
The machine is built by the manufacturer and supplied directly, with no trading intermediary between the works and the buyer. The tooling comes out of the manufacturer’s own archive of floor deck profiles, which covers both open and closed deck geometry, so a profile already in that archive is a known die set rather than a new development.
♦ COMPANY PROFILE:
Hebei Xinnuo Roll Forming Machine Co., Ltd., not only produce different types of professional roll forming machines, but also develop intelligent automatic roll forming production lines, C&Z shape purline machines, highway guardrail roll forming machine lines, sandwich panel production lines, decking forming machines, light keel machines, shutter slat door forming machines, downpipe machines, gutter machines, etc.
There are several advantages of using roll forming for your projects:
- The roll forming process allows operations such as punching, notching, and welding to be performed in-line. Labor cost and time for secondary operations are reduced or eliminated, reducing part costs.
- Roll form tooling allows for a high degree of flexibility. A single set of roll form tools will make almost any length of the same cross-section. Multiple sets of tools for varying length parts are not required.
- It can provide better dimensional control than other competing metal forming processes.
- Repeatability is inherent in the process, allowing easier assembly of roll formed parts into your finished product, and minimizing problems due to “standard” tolerance build up.
- Roll forming is typically a higher speed process.
- Roll forming offers customers a superior surface finish. This makes roll forming an excellent option for decorative stainless steel parts or for parts requiring a finish such as anodizing or powder coating. Also, texture or pattern can be rolled into the surface during forming.
- Roll forming utilizes material more efficiently than other competing processes.
- Roll formed shapes can be developed with thinner walls than competing processes
In modern construction and manufacturing, the roll forming machine (commonly known as a roof tile or sheet metal roll former) has revolutionized profile fabrication. By replacing labor-intensive traditional press brake methods, advanced roll forming technology offers unmatched efficiency, quality, and cost savings for metal roofing and wall panel production.
Here are the key advantages of implementing a modern roll forming machine in your operations:
1. Unmatched High Efficiency and Output Speed
High-speed roll forming lines operate continuously, producing custom metal panels at speeds up to 20–40 meters per minute. This automated process significantly shortens lead times and accelerates project delivery cycles.
2. High Precision and Consistent Quality
Engineered with heavy-duty steel frames, high-precision roller dies, and PLC automated control systems, roll formers deliver pinpoint dimensional accuracy. Every panel exhibits uniform thickness, sharp profiles, and precise hole punching, ensuring seamless job-site installation.
3. Material Efficiency and Reduced Waste
Continuous roll forming minimizes scrap metal generation compared to conventional stamping. Precise coil feeding and automated hydraulic flying shears ensure optimal material utilization and reduced raw material costs.
4. Low Maintenance and Extended Durability
Constructed with heat-treated chrome-plated rollers and robust drive systems, industrial roll forming machines require minimal downtime while delivering a long service life under heavy daily operation.
Conclusion
Investing in a reliable roll forming machine boosts productivity, lowers labor costs, and guarantees consistent product quality—delivering maximum long-term return on investment (ROI) for metal fabrication businesses.
Metal roll forming is a continuous, automated metal fabrication process used to shape long strips of sheet metal (usually coiled steel or aluminum) into specific, uniform cross-sectional profiles.
Unlike traditional metal bending techniques like press braking—which shapes sheets batch by batch—roll forming operates as a continuous production line, making it one of the most efficient manufacturing methods for structural profiles, roofing panels, and automotive components.
How the Metal Roll Forming Process Works
The process passes coil stock through a series of consecutive roller dies to incrementally shape the metal into a finished cross-section:
-
Uncoiling: A heavy coil of sheet metal (often pre-painted, galvanized, or stainless steel) is mounted onto a decoiler and fed continuously into the line.
-
Progressive Forming: The strip passes through a sequence of mating roller stations (known as flower patterns). Each set of rollers gradually bends the metal by a few degrees. By making incremental bends, the process avoids overstressing the material or cracking protective coatings.
-
In-Line Processing (Optional): Pre-punching, post-punching, slitting, or embossing can be integrated directly into the automated line before or after forming.
-
Cutting to Length: Once the final profile is shaped, an automated flying shear or hydraulic cutter cuts the continuous panel into precise custom lengths without interrupting the line speed.
Key Advantages of Metal Roll Forming
-
Continuous High Output: Roll forming lines operate at high speeds (typically 20–50 meters per minute), significantly outperforming press brakes for mass production.
-
Tight Dimensional Tolerances: Advanced PLC automation and precision-machined rollers ensure strict dimensional consistency across every piece produced.
-
Material & Cost Efficiency: Minimizes scrap metal waste and eliminates extra handling steps by integrating punching, bending, and cutting into a single automated line.
-
Design Flexibility & Surface Protection: Capable of producing complex, multi-bend profiles while preserving surface finishes, galvanization, and paint coats.
Common Applications
Metal roll forming is widely used across multiple heavy-duty industries:
| Industry | Common Roll-Formed Products |
| Building & Construction | Trapezoidal roof tiles, standing seam panels, C/Z purlins, drywall studs, rain gutters |
| **Automotive &# What is Metal Roll Forming? |
Metal roll forming is a continuous, high-volume manufacturing process that bends long strips of sheet metal—usually coiled steel or aluminum—into custom cross-sectional profiles.
Unlike traditional press braking or stamping, which processes metal in single discrete batches, roll forming shapes metal incrementally at room temperature (cold forming) through a series of consecutive roller dies.
How Metal Roll Forming Works
The roll forming process relies on a line of paired roller stations that gradually shape the metal in steps:
-
Coil Unloading & Uncoiling: A heavy coil of flat metal strip is loaded onto an uncoiler and fed continuously into the machine.
-
In-Line Pre-Punching: Automatic presses notch, punch holes, or create slots in the flat strip prior to shaping.
-
Progressive Roll Shaping: The strip passes through multiple sets of upper and lower rollers (called roll stations). Each station bends the metal slightly more than the previous one, preventing stress fractures and material strain.
-
Cutting & Shearing: A flying hydraulic shear cuts the finished profile to exact target lengths without stopping the continuous line.
Key Benefits of Roll Forming
-
High Speed & Efficiency: Lines operate at speeds up to 20–50 meters per minute with minimal manual labor required.
-
Consistent Quality & Precision: Heavy-duty tool steel rollers controlled by PLC automation ensure exact tolerances across thousands of identical panels.
-
Material Waste Reduction: Continuous coil processing generates virtually zero scrap compared to conventional sheet stamping or trimming.
-
Complex Profiles: Produces intricate shapes—such as standing seam panels, hat channels, C/Z purlins, and tubular sections—in a single continuous pass.
Common Applications
-
Building & Construction: Roof tiles, wall cladding panels, gutters, structural purlins, and steel framing studs.
-
Automotive: Bumper beams, door impact bars, and chassis structural rails.
-
Solar & Energy: Solar panel mounting racks and support structures.
-
Storage & Industrial: Warehouse racking systems, shelving, and heavy-duty tracks.
-
Heavy Duty Cold Roll Forming Machine | High-Str...
-
Floor Decking Panels Roll Forming Machine iron ...
-
Floor Decking Panels Roll Forming Machine iron ...
-
Galvanized Steel Floor Deck Machine | Hydraulic...
-
Automatic Floor Deck Roll Forming Machine | Hig...
-
floor tile making machine for sheet metal profi...